- This topic is empty.
-
AuthorPosts
-
27/10/2026 at 18:14 #12855
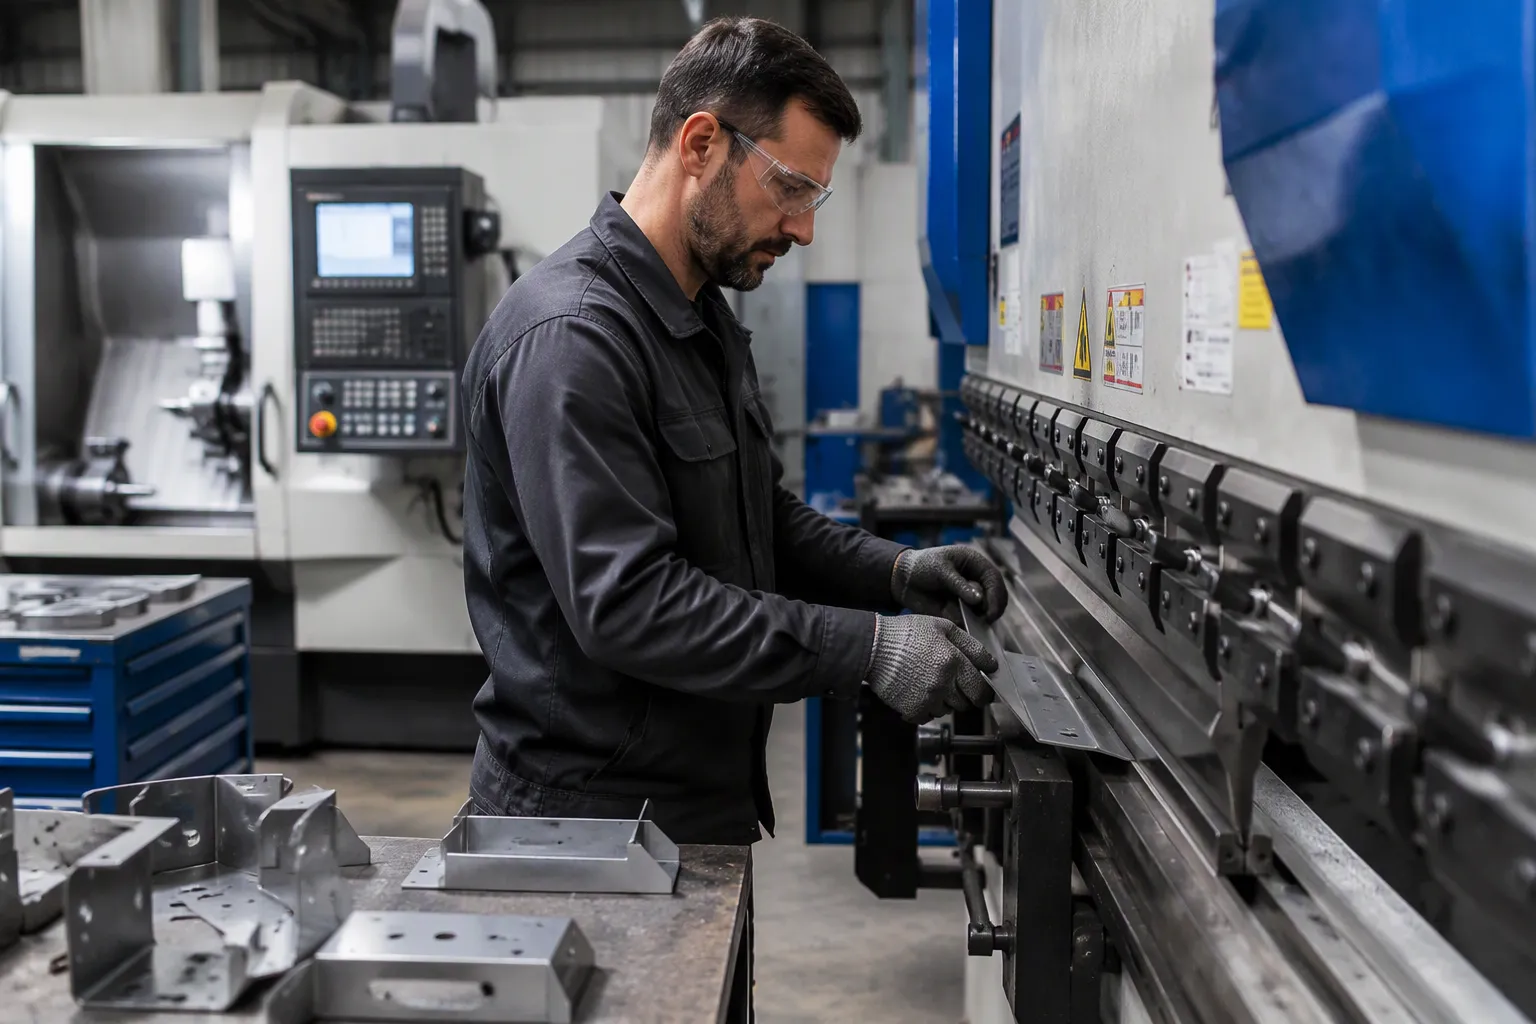
Image Source: https://www.xuxiangtaimetal.com Write a professional sheet metal fabrication cuts, forms, and joins flat sheet into custom metal parts built to a drawing. Enclosures, brackets, chassis, and mounting hardware rely on this route for strength-to-weight, repeatability, and cost at volume. Process choice, material thickness, part geometry, and tolerances work as one decision set.
Key Takeaways
- Choose cutting and bending methods based on metal thickness and precision needs.
- Keep holes and features away from bends to prevent distortion.
- Specify tight tolerances only where they are truly needed to save cost and time.
Sheet Metal Fabrication Processes at a Glance
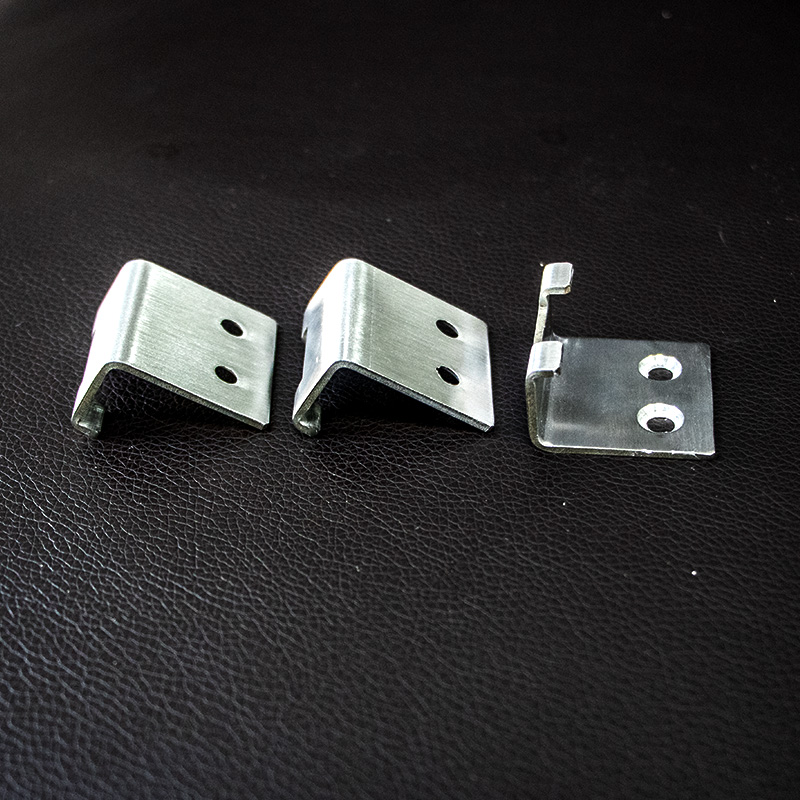
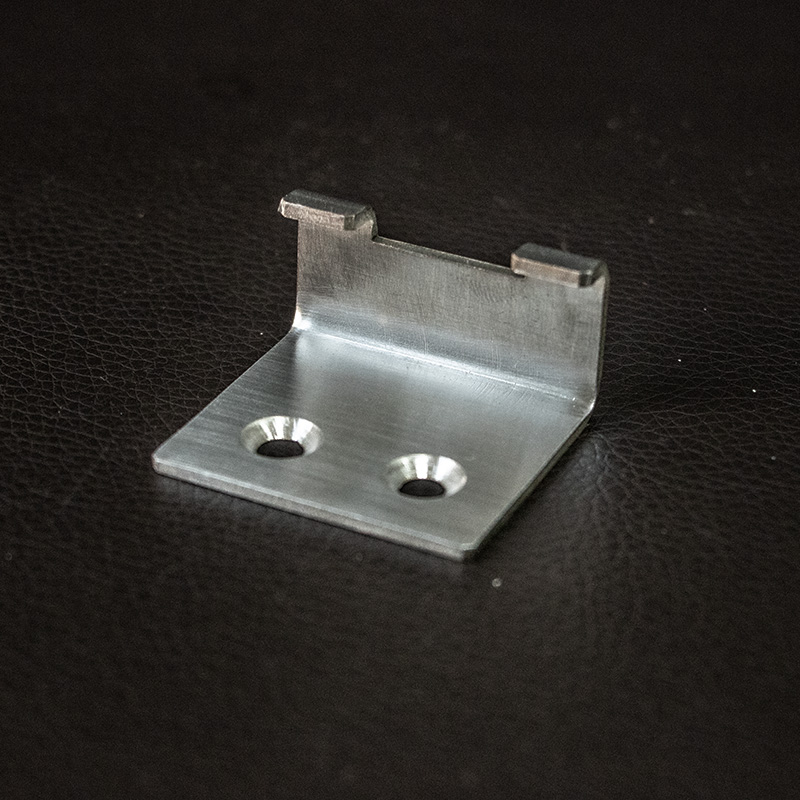
Custom sheet metal parts move through a sequence of operations. Each operation changes the flat sheet in a specific way. Cutting separates material. Bending and forming create three-dimensional geometry. Punching adds holes and features. Joining connects separate pieces into one assembly. Surface finishing protects the part and improves its appearance. A fabricator selects and sequences these operations based on the part drawing, material, and production volume.
Cutting: Laser, Plasma, and Shearing
Cutting is the first step in most sheet metal projects. The fabricator takes a flat sheet and separates it into blanks or cuts internal features. Three methods dominate this stage: laser cutting, plasma cutting, and shearing.
Laser cutting uses a focused beam of light to melt and vaporize metal. The process delivers exceptional precision. Kerf width—the gap left by the cut—measures about 0.4 mm with laser cutting. This narrow kerf allows intricate shapes and tight nesting of parts on the sheet. Laser cutting excels on thin sheet metal, typically under 10 mm. The cut edge comes out clean and largely burr-free. A fiber laser system carries a high startup cost, but its speed and automation deliver favorable operating economics for high-volume thin precision work.
Plasma cutting uses an electrically conductive gas to create a high-temperature plasma arc. The arc melts the metal and a gas jet blows the molten material away. Plasma cutting produces a wider kerf of about 3.8 mm. The edge quality is rougher, with more dross and a larger heat-affected zone. Secondary finishing may be necessary. The equipment costs significantly less than a laser system—a 5’x10′ heavy-duty table runs around $100,000. Plasma cutting shines on thick conductive metals, often above 1 inch, where low operating cost matters most.
The initial investment for a plasma cutting machine is typically 2-5 times less than a fiber laser cutting system. While that may seem like a one-time cost, the depreciation charges significantly increase the fiber laser system’s total cost of ownership (TCO) for years. For direct operating costs, plasma typically costs less per foot/meter for thicker materials, while fiber laser direct operating costs are lower for thin metals but incur higher electricity and gas consumption.
The table below summarizes the key differences between the two methods.
Attribute Laser Cutting Plasma Cutting Precision (tolerance) Very high, ±0.002″ Wider kerf (~3.8 mm), less precise edges Best material range Thin sheet metal (<¼″) Thick conductive metals (>1″) Startup/equipment cost High startup cost Lower equipment cost (~$100,000 for 5’x10′ HD table) Operating economics Favorable for high-volume thin precision work Cost-efficient for thick, large-scale production Edge quality Clean, burr-free, minimal post-processing More dross, larger heat-affected zone, secondary finishing may be needed Shearing is a third cutting option. A shear machine uses a straight blade to cut sheet metal along a line. Shearing works best for straight cuts on flat sheets. The process is fast and cost-effective for simple rectangular blanks. Shearing cannot produce curves or intricate internal features. Fabricators often use shearing for initial sheet breakdown before other cutting operations.
Bending and Forming: From Flat Blank to 3D Geometry
Bending transforms a flat blank into a three-dimensional part. A press brake holds the sheet between a punch and a die. The punch presses the material into the die, creating a bend along a straight line. The angle of the bend depends on how far the punch travels into the die.
Three bending methods exist: air bending, bottoming, and coining. Air bending is the default method. The punch depth controls the bend angle, and the sheet does not press fully against the die walls. One tool set can produce any angle—30°, 90°, or 120°—without tool changes. Air bending produces the most springback, which the operator compensates for by overbending. Bottoming presses the sheet against the die walls. The die angle sets the part angle, which reduces springback and improves repeatability. Bottoming requires a dedicated tool set for each angle. Coining forces the metal fully into the die, plastically deforming it through the full thickness. Coining produces almost no springback and the tightest radii, but it demands several times the tonnage of air bending. Coining is a specialist choice, not a default.
Method How the bend angle is set Springback behavior Tooling/tonnage implications Air bending (default) Punch depth controls angle; sheet not pressed to die bottom Springs back the most; compensated by overbending One tool set produces any angle; no tool changes for 30°/90°/120° bends Bottoming Sheet pressed against die walls; die angle sets part angle Less springback, more repeatable Requires a dedicated tool set per angle Coining Metal forced fully into die, plastically deforming through full thickness Almost no springback; tightest radii Several times the tonnage; specialist choice, not default Springback is the elastic recovery that causes a bend to open slightly after the punch lifts. Only part of the deformation is plastic, so the material springs back toward its original shape. Springback worsens with harder material, thicker material, and larger bend radii. The standard compensation is overbending—the brake bends past the target angle so the part relaxes into the specified angle. Fabricators establish exact compensation on the shop floor through first-article testing rather than calculating it on paper.
Bend radius selection follows a few practical rules. The inside bend radius should at least equal the sheet thickness as a safe starting point. Ductile materials like 5052 aluminum and mild steel tolerate tighter radii. Hard or tempered materials like 6061-T6, stainless steel, and hardened steel require a more generous radius because tight radii risk cracking. Thicker material needs a proportionally larger radius. Designers should use a single radius throughout the part to reduce tooling setups and cost.
Condition Recommended bend radius guidance General safe starting rule Inside bend radius should be at least equal to the sheet thickness Ductile materials (e.g., 5052 aluminum, mild steel) Tolerate tighter radii Hard/tempered materials (e.g., 6061-T6, stainless, hardened steel) Require a more generous radius; tight radii risk cracking Thicker material Needs a proportionally larger radius Design consistency Use a single radius throughout the part to reduce tooling setups and cost Other forming operations extend beyond simple bending. Stamping and stretching plastically deform sheet metal into complex shapes. Rolling and rounding bend sheet metal into cylinders or arcs. Riveting and pre-riveting press nuts and screws into sheet metal holes during the forming phase, which simplifies final assembly.
Punching and Hole Making
Punching creates holes and features in sheet metal using a punch and die. A CNC punch press drives the punch through the sheet and into the die. The process is fast and efficient for high-volume production. Stamping performs similar operations—blanking, punching, grooving, and embossing—using dies for standardized mass production.
Hole size and shape depend on the punch and die tooling. The punched feature should be no smaller than the material thickness as a rule. For CNC punching, the minimum hole diameter should be no less than 1.2 times the material thickness to avoid punch deformation. The die is made slightly larger than the punch—typically about 10% of material thickness—to reduce tooling wear and punching pressure. For example, a 1.000″ punch for 0.100″ aluminum would use a 1.010″ die. Hole size on the punch side matches the punch; on the die side it matches the die. Hole-to-hole variation stays minimal aside from tooling wear.
Typical CNC punching tolerances run approximately ±0.2 mm unless precision ground tooling is used. A generally reasonable functional tolerance is ±0.003″. For hole-to-edge distance, ±0.010″ is recommended, with ±0.005″ used only when necessary. For hole-to-bend distance, ±0.015″ is functionally reasonable for most applications, with ±0.010″ reserved for critical cases.
Feature Typical Tolerance (mm) Notes Linear Dimension (General) ±0.1 to ±0.5 Depends on die precision and material thickness Hole Diameter ±0.1 to ±0.2 Depends on die condition; smaller holes tend to have tighter tolerances Hole Position ±0.13 to ±0.25 Single punches are highly precise; cumulative error can occur over a series of punches Welding, Riveting, and Mechanical Joining
Joining connects separate sheet metal components into a single assembly. Three main approaches exist: welding, riveting, and mechanical fastening. Each method suits different applications.
Welding joins parts using spot, arc, or laser welding. Welded joints typically achieve 90-100% joint efficiency. Properly executed welds match or exceed base material strength. Welding suits structural loads, frames, enclosures, tanks, and load-bearing assemblies. The process is typically faster and more cost-effective at production volumes, especially with automation. Welding does carry higher equipment and training costs. The heat-affected zone may cause distortion in thin materials.
Riveting fixes parts together using rivets. Riveted joints reach about 60-80% joint efficiency. Riveted joints are weakened by stress concentrations around fastener holes. Riveting offers flexibility, is easy to inspect, and works well with delicate materials. The method proves valuable for aerospace and repair work. Riveting is more labor-intensive but has lower equipment costs. It suits tight budgets, short timelines, and simple, non-load-bearing structures. Riveting also performs well in vibration-prone applications because joints can be inspected and replaced.
Factor Welding Riveting Strength Very high; suited to structural loads Moderate; depends on rivet type and spacing Cost Higher labor and skill cost Generally lower cost Speed Slower for precision welds Fast assembly Aspect Riveting Welding Strength behavior Strong under shear loads; preserves base metal properties Strong under tensile and shear loads; can match or exceed base material strength Labor & cost Less skill required; faster for high-volume assembly Skilled operators needed; higher equipment and training costs Best use case Vibration-prone applications (aerospace, transport); joints can be inspected/replaced Permanent structural assemblies (frames, tanks); heat-affected zone may cause distortion Cost drivers Low-cost equipment, minimal training, fast cycle times Higher equipment costs (power supplies, shielding gas, fixtures) Mechanical fastening—bolted and other fastened construction methods—rounds out the joining options. Mechanical fasteners allow disassembly and reassembly, which suits maintenance-heavy applications. The best joining choice depends on material type, required joint strength, production quantity, and maintenance plans.
Surface Finishing and Deburring
Surface finishing removes burrs, prepares the surface, and applies protective or decorative coatings. Deburring is often the first finishing step. Laser-cut and punched parts carry sharp edges and burrs that require removal. Manual deburring uses swivel tools, files, wire wheels, and countersinks to meet specific requirements. Linear deburring handles large flat parts and removes mill markings and surface burrs quickly and cost-effectively. Tumbling processes smaller parts, lightly rolls edges, and prepares parts for further processing or plating. Media blasting preps surfaces for paint and powder coat adhesion; bead blasting before anodizing produces a matte finish.
Coating and plating follow deburring and cleaning. Powder coating covers metal with a thin organic film for decorative and protective purposes. It improves resistance to weather, heavy usage, and corrosion with longer durability than liquid paints. Metal plating covers a surface with a thin film of another metal—nickel, silver, gold, chrome, or zinc—to add durability, increase corrosion resistance, and improve appearance. Anodizing builds an oxide layer on aluminum, titanium, zinc, and magnesium to increase corrosion resistance and visual appeal. Chromate conversion coating best serves functional parts; it protects from corrosion and acts as a paint primer.
Finishing Method Typical Applications Linear Deburring Large flat parts needing improved visual appearance over raw stock; cost-effective and fast, removes mill markings and surface burrs Tumbling Smaller parts requiring lightly rolled edges and improved surfaces; prepares parts for further processing or plating and enables safe handling/assembly Media Blasting Prepping surfaces for paint and powder coat adhesion; bead blasting before anodizing produces a matte finish Sanding Large flat surfaces needing uniform, durable finishes; also used for touch-up repairs of minor damage Straight Graining Cosmetic unidirectional grain finish similar to stainless appliances or commercial fixtures Polishing High-gloss reflective surfaces; usually the final step after progressively finer sanding Manual Deburring Touch-up work using swivel tools, files, wire wheels, and countersinks to meet specific requirements Finish Application Bead Blasting Mainly visual purposes and preparing surfaces for other coatings; can be combined with anodizing Powder Coating All metals; both decorative and protective; can be combined with bead blasting Anodizing Aluminum, titanium, zinc, and magnesium to increase corrosion resistance and visual appeal Chromate Conversion Coating Best for functional (not decorative) parts; protects from corrosion and acts as a paint primer Brushing Aesthetic purposes; covers up machining imperfections on customer-facing parts Brushing + Electropolishing Parts needing microscopic-level smoothness; mostly used for stainless steels Brushed metal finishes use special abrasive brushes to remove imperfections and recover functionality on damaged parts. Brushing also creates a granular, scratched texture on external surfaces. Metal polishing produces glossy surfaces on stainless steel, copper, or aluminum. Polishing smooths parts before plating and restores old or neglected metal surfaces. Sand blasting hits metal surfaces with a jet of fine abrasive material to make stainless or carbon steel matt, more corrosion-resistant, and clean from impurities. Sand blasting typically precedes painting.
Selecting Materials for Custom Sheet Metal Parts
Material selection anchors every downstream decision in a sheet metal project. The chosen alloy, temper, and thickness determine which cutting method suits the blank, how tightly the part can bend, and which joining process holds the assembly together.
Common Metals Compared: Steel, Stainless, and Aluminum
Carbon steel offers high strength at low cost, good weldability, and reliable formability in low-carbon grades. Uncoated carbon steel resists corrosion poorly, so it needs paint, plating, or powder coating. Stainless steel delivers high strength and excellent corrosion resistance through its chromium-rich passive oxide layer. Grade 304 suits food-processing equipment, medical devices, and architectural panels. Grade 316 adds molybdenum for better chloride resistance in marine and chemical environments. Aluminum provides an excellent strength-to-weight ratio at roughly one-third the density of steel. Grade 3003 forms easily, 5052 combines strength with good bending performance, and 6061-T6 runs stronger but less forgiving at tight radii.
Material Key properties Typical applications Carbon steel High strength, low cost, good weldability, poor corrosion resistance uncoated Brackets, panels, enclosures, frames Stainless steel High strength, excellent corrosion resistance, hygienic surface Food equipment, medical devices, marine hardware Aluminum Excellent strength-to-weight ratio, good corrosion resistance, non-magnetic Aerospace structures, electronic enclosures, lightweight panels Matching Material Thickness to Function
Thickness governs forming force, bend radii, minimum flange dimensions, part weight, and tooling requirements. A gauge that laser cuts easily may still challenge forming when the part carries short flanges or tight bends. Designers should size tabs at least 2 × t, notches no narrower than 1.5 × t, and relief cuts at least 1 × t. Holes and slots should match or exceed material thickness. Typical fabrication handles 0.9 mm to 20 mm stock.
A heavier gauge adds strength but alters cutting and forming behavior, so bends, flanges, and ribs often achieve rigidity more economically than simply increasing thickness.
Material Choice and Its Effect on Process Selection
Alloy and temper set feasible bend radii and springback. Ductile grades tolerate greater forming strain with lower crack risk. Thicker sheet demands more forming force and larger tooling. Heat-sensitive alloys may call for waterjet cutting to avoid a heat-affected zone, while thin-gauge precision work favors fiber laser. Bending perpendicular to grain direction reduces cracking risk at tight radii. High-volume programs justify dedicated stamping dies, while low or variable volume favors flexible press-brake forming.
Designing Industrial Components for Manufacturability
A manufacturable part starts on the drawing, not on the shop floor. Designers who understand how sheet metal behaves during cutting and forming avoid the small geometry choices that drive rework, scrap, and cost. Three design areas matter most: bend geometry, feature placement near bends, and the discipline of standardizing thicknesses and trimming unnecessary features.
Bend Radii, Bend Relief, and Springback
Bend radius sets the foundation for every formed feature on a part. A tight radius concentrates strain on the outer fiber of the bend. Ductile metals tolerate this strain. Hard or tempered alloys crack under it. Designers should start with an inside bend radius equal to the sheet thickness and increase the radius for harder alloys, thicker stock, and parts that will see fatigue loading. A single consistent radius across the part reduces tooling changes and shortens setup time.
Bend relief protects the part where a bend terminates at an edge or meets an opening. Without relief, the material tears or distorts at the bend root. The relief is a small cut—rectangular or rounded—placed at the end of the bend line. Its width and depth depend on material thickness, material type, and bend radius. For general applications, the relief can run slightly wider than the material thickness, with depth extending just beyond the bend region.
Cutting Method Minimum Relief Width Inset / Depth Rule Shape Laser-cut parts At least 0.015 in (0.381 mm) Inset 0.015 in (0.381 mm) from the bend radius Rectangular or rounded Router-cut parts (e.g., bent aluminum with machined features) About half the material thickness, but no smaller than 0.045 in (1.143 mm) Depth should extend just beyond the bend radius Rounded Designers should watch for stress concentration where a bend line intersects an opening, slot, or internal hole. Notch-sensitive materials—stainless steel, high-strength steel, and titanium—demand special care at the bend root. Sharp notches in these alloys act as crack starters. A rounded relief with generous width removes that risk.
Springback complicates every bend. The material elastically recovers after the punch lifts, so the finished angle opens slightly from the commanded angle. Harder alloys, thicker stock, and larger radii all increase springback. The press brake operator compensates by overbending, and the exact compensation is established through first-article testing rather than calculated on paper. Designers help by avoiding bend angles that sit at the edge of a press brake’s capability and by keeping radii consistent so the operator can dial in one compensation value for the whole part.
Hole and Feature Placement Relative to Bends
Holes placed too close to a bend line deform during forming. The material stretches in the bend zone, and any hole inside that zone ovals or tears into a teardrop shape. A distorted hole is a reject for tapped holes, shoulder-bolt holes, and mating patterns. The fix is distance: designers must keep hole edges far enough from the bend line that the deformation zone never reaches them.
The minimum distance follows a simple formula. For small holes under about 1 inch (25 mm) in diameter, the hole-edge-to-bend-line distance equals 2T + R, where T is material thickness and R is the inside bend radius. For large holes and slots at or above 1 inch, the formula steps up to 2.5T + R. A simplified shop rule keeps holes at least 3T from the bend line, and conservative DFM guides push clearance to 3–4T from the bend zone.
Feature size Minimum hole-edge-to-bend-line distance Small holes (< ~1 in / 25 mm dia.) d = 2T + R Large holes & slots (≥ ~1 in / 25 mm) d = 2.5T + R The table below converts the formula into working distances for common steel gauges, assuming an inside bend radius equal to the material thickness.
Steel gauge Thickness T (in) Small holes/slots < 1 in: 2T + R Large holes/slots ≥ 1 in: 2.5T + R 18 ga 0.048 0.144 in 0.168 in 16 ga 0.060 0.180 in 0.210 in 14 ga 0.075 0.225 in 0.263 in 12 ga 0.105 0.315 in 0.368 in 11 ga 0.120 0.360 in 0.420 in 10 ga 0.135 0.405 in 0.473 in 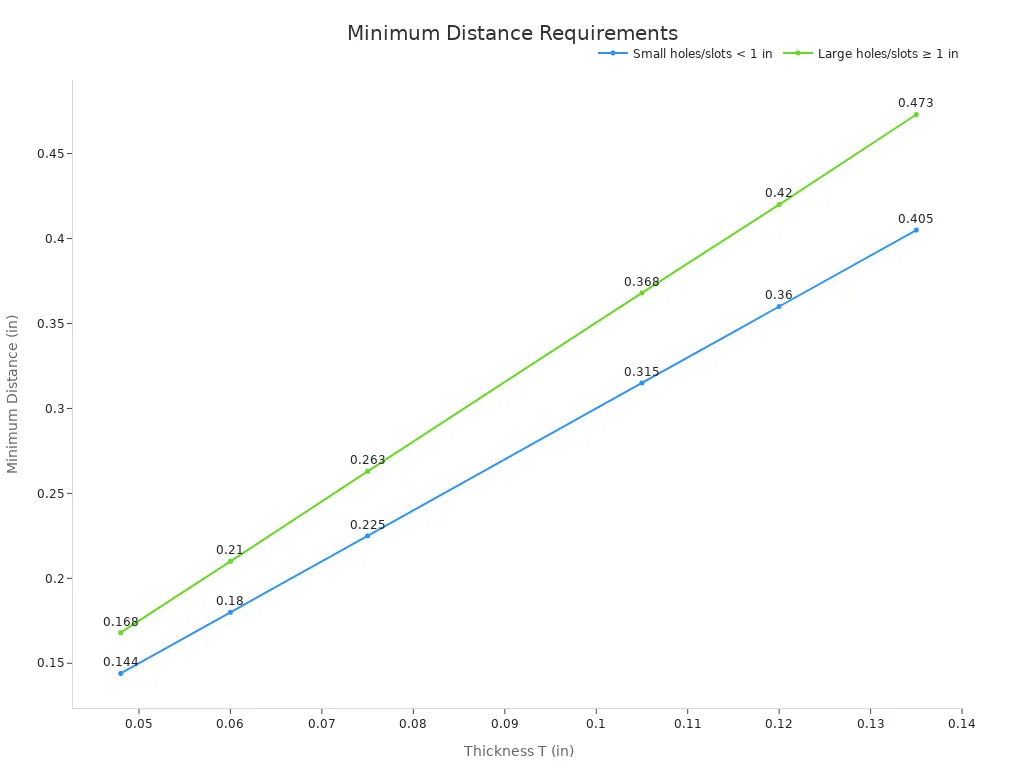
Image Source:https://www.xuxiangtaimetal.com The 2T + R rule applies regardless of cut method. Laser cutting does not relax hole-to-bend clearance because the problem is forming, not cutting. Slots are more sensitive to bend distortion than round holes, which is why the formula steps up to 2.5T + R for slots and large features. Some shops push slots to 4T + R near a bend to add margin. Designers who place features with these distances in mind avoid the most common cause of first-article rejection.
Standardizing Thicknesses and Reducing Features
Sheet metal is stocked in standard gauges. A design that specifies a non-standard thickness—0.105 inch instead of the adequate 0.109 inch (12 gauge)—forces custom ordering, premium pricing, and extended lead times. Standard gauges available from distributor stock typically reduce material cost by 15–25% and improve lead time predictability. The savings compound across a production program.
Standardizing thicknesses delivers several practical benefits. Purchasing can buy materials in bulk, which lowers per-unit material cost. Setup time during fabrication drops because the shop runs the same tooling and machine settings across more parts. Fabrication processes simplify overall, and scheduling becomes more predictable.
Reducing features follows the same logic. Every hole, notch, bend, and cutout adds a tooling step, a setup, or a machine cycle. Designers should ask whether each feature serves a function. Cosmetic holes, redundant mounting points, and decorative cutouts add cost without adding value. Consolidating similar hole sizes lets the shop use one punch tool. Aligning features to a common grid reduces machine travel. Grouping bends in the same direction lets the operator form the part in fewer hits.
A disciplined design review catches these opportunities before the drawing reaches the shop. The review checks bend radii against material, verifies relief at every bend termination, confirms hole-to-bend distances, and audits thicknesses against standard gauge stock. Each correction at the drawing stage costs minutes. The same correction after the first article costs tooling time, scrap material, and schedule delay.
Tolerances and Technical Drawings for Metal Fabrication
Tolerances define how much a finished part may deviate from its drawing. Technical drawings communicate those limits to the fabricator. Together, they determine whether a custom sheet metal part fits its assembly on the first attempt.
What Drives Achievable Tolerances
Achievable tolerance depends on the material, the tooling, and the forming sequence. Material type and mechanical properties set the baseline precision. Elasticity and springback cause the sheet to return partially toward its original shape after the load releases, so the finished angle deviates from the target. Thickness, rigidity, and rolling direction all shift forming behavior. Equipment, dies, punch clearance, and operation sequence add accumulated variation. Heat treatment and surface coatings can move dimensions after forming.
Factor Category Specific Factors Effect on Achievable Tolerance Workpiece Material type and mechanical properties Sets the baseline precision Workpiece Elasticity and springback Causes angle and dimension deviation Workpiece Thickness, rigidity, rolling direction Shifts formability and springback magnitude Production resources Equipment, tools, dies, presses Limits repeatable accuracy Production resources Operation sequence, heat treatment, coatings Accumulates variation and post-process shift Sheet-metal specific Bend radii, flat-pattern calculation, die clearance Controls angle and final dimensions Springback is a fundamental driver of achievable tolerance in bending. Specifying only a final angle is insufficient. The material’s response during processing must be evaluated and compensated through correct flat-pattern calculation and bend-radius selection.
Datum and Tolerance Callouts That Prevent Rework
Datums should mirror how the part is manufactured and assembled, not how it was modeled in CAD. Designers derive datum features from manufacturing and assembly surfaces. The datum order in the feature control frame reflects the sequence in which the part is constrained.
- Specify tolerances only where they are functionally required.
- Reserve tight geometric tolerances for bearing bores, dowel pin holes, mating faces, and sealing surfaces.
- Assign general tolerances to clearance holes and noncritical features.
- Use ISO 2768 or title-block defaults for noncritical dimensions.
- Perform tolerance stack-up analysis before locking tolerances.
- Choose large, stable primary datums that are accessible for measurement.
What a Fabricator Needs to Quote Custom Metal Parts
A complete quote package lets the fabricator plan nesting, cutting, forming, and finishing without back-and-forth. The drawing set should include orthographic views, a 2D flat pattern with reference dimensions, and full dimensions for every bend, hole, countersink, flange, and formed feature. Dimension to virtual intersection points and show included bend angles. Specify sheet stock size and preferred suppliers, since thickness tolerance varies by manufacturer. Add hardware installation details, finishing specifications, weld symbols, masked areas, and part marking callouts. Submit CAD files or technical drawings together with material requirements, production quantities, and project specifications. The fabricator then reviews these requirements and recommends the appropriate fabrication approach.
Surface Finishing for Service Conditions
Image Source: https://www.xuxiangtaimetal.com A finish must solve a functional problem. Appearance matters, but the operating environment dictates the complexity of the coating system. Designers who specify finish by service condition avoid premature corrosion, wear failures, and costly field repairs.
Powder Coating, Painting, and Plating
Powder coating applies a thin organic film that resists weather, heavy usage, and corrosion. The coating outlasts liquid paint in most outdoor applications. Liquid painting remains a practical choice for large assemblies and touch-up work. Plating deposits a thin layer of another metal, such as zinc, nickel, or chrome, to add durability and corrosion resistance. Anodizing builds an oxide layer on aluminum and titanium for the same purpose. Chromate conversion coating protects functional parts and acts as a paint primer.
Specifying Finish by Operating Environment
The service environment sets the finish specification. A dry indoor part may need only a brushed finish or basic plating. Outdoor exposure to rain, UV, and humidity calls for powder coating, anodizing, or zinc plating. Marine and high-corrosion settings demand hot-dip galvanizing, electropolishing with passivation, or multi-layer coating systems. High-temperature and high-wear conditions favor hard chrome, electroless nickel, or thermal-resistant finishes.
Operating Environment Recommended Surface Finish Indoor dry Brushed finish, light polishing, basic plating Outdoor exposure (rain, UV, humidity) Powder coating, anodizing, zinc plating Marine / high corrosion Hot-dip galvanizing, electropolishing + passivation, multi-layer coating systems High temperature / industrial wear Hard coatings (chrome, nickel), thermal-resistant finishes Selection should also weigh UV and weathering exposure, chemical or fluid contact, abrasion loads, and high-temperature oxidation. A finish that does not solve a functional problem is not the correct finish.
OEM Manufacturing and Fabricator Communication
Clear communication between the OEM and the fabricator determines whether a custom sheet metal program runs smoothly. Drawings, samples, and specifications carry the design intent. Early review turns that intent into a repeatable production process.
Working From Drawings, Samples, and Specifications
A complete package gives the fabricator everything needed to plan the build. Buyers should follow a few practical steps when preparing that package.
- Select materials wisely. Match metal strength, tolerance, and appearance to the project, and collaborate early with the fabricator to avoid costly design flaws.
- Prefer the coil-fed approach where possible. It is generally more productive and consistent and generates less waste than cut-length sheet processing.
- Verify tooling and equipment condition. Request preventive-maintenance records and repeatability documentation to limit downtime and protect part quality.
- Assess part complexity. Complex profiles raise tooling cost and slow run speeds, so consult the provider early for concurrent design input.
- Loosen tolerances and respect bend radii. Use functional tolerancing instead of blanket title-block tolerances, since over-tight tolerances drive up tooling cost, lead time, and material grade requirements.
Designs must also keep consistent sheet thickness so bending and forming behave predictably. The appropriate bend radius depends on material, thickness, and forming process, and the fabricator should confirm it rather than assume a universal rule. Holes placed too close to bends or edges deform during forming, and relief cuts reduce stress and tearing where bends approach edges.
Consideration Area Key Requirements to Specify CAD / 3D models Compatible formats such as STEP, IGES, DXF, DWG 2D drawings Fully dimensioned drawings for every feature Material Type and grade explicitly stated Tolerances General tolerances plus critical dimensions needing tighter precision; avoid blanket tight tolerances GD&T Geometric dimensioning and tolerancing callouts where needed Surface finish / coating Finish type, protective coatings, color specs (RAL/Pantone) Inspection & compliance FAI/CMM inspection, industry standards, material certifications Project context Quantity (prototype vs. production), volume, lead time, delivery, budget, DFM openness Early Design Review and Repeatable Production
Early design review gives the OEM room to change before drawings, suppliers, tooling, fixtures, work instructions, and inspection plans are finalized. Engineering and quoting teams review drawings, tolerances, and materials together with the OEM’s technical team before production starts. This collaboration produces manufacturing routers and work instructions tuned for the floor, reduces rework, and protects design intent across the full build.
A manufacturable design is one that can be produced repeatedly with acceptable cost, quality, lead time, and process control, not merely made once. DFM review flags issues that hinder scaling, such as excessive setup time, hard-to-source materials, unnecessary tolerances, specialized fixturing, and extra inspection. Feedback from prototype, pilot, and early production builds refines the design package and confirms process assumptions for repeatable manufacturing. Stable manufacturing systems lower operational costs and simplify scaling production as demand grows.
Manufacturable custom sheet metal parts come from aligning material, geometry, tolerances, and finish at the design stage, not after the first article. Early fabricator involvement reduces rework, quoting delays, and cost surprises in OEM manufacturing programs. Qingdao Xuxiangtai Machinery Manufacturing Co., Ltd. supports custom manufacturing based on customer drawings, samples, and technical specifications. Readers can share component drawings and manufacturing requirements to discuss suitable fabrication approaches.
FAQ
Which sheet metal process suits thin precision parts?
Laser cutting handles thin precision blanks best. Press-brake bending then forms the part. Fiber laser systems deliver narrow kerf and clean edges on stock under 10 mm.
How does a buyer specify tolerances without driving up cost?
A buyer reserves tight tolerances for functional features only. General tolerances cover clearance holes and noncritical dimensions. This approach controls tooling cost and lead time.
What should a drawing package include for an accurate quote?
The package needs orthographic views, a flat pattern, bend angles, hole callouts, material grade, finish specs, and quantity. Complete data lets the fabricator plan nesting and forming without clarification delays.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.