- This topic is empty.
-
AuthorPosts
-
21/10/2026 at 17:19 #12782
Image Source: https://www.xuxiangtaimetal.com Qingdao Xuxiangtai operates an integrated custom metal plant in Jimo, Qingdao. Casting, CNC machining, sheet metal fabrication, and metal 3D printing run under one roof. The 26,200 m² facility brings 20+ years of export experience, 130+ international clients, and 460+ completed projects. Every order includes 100% dimensional inspection, spectral material validation, and NDT reports (PT, RT, pressure testing), backed by IATF 16949 and RoHS. US buyers receive English communication and after-sales engineering support. Buyers planning a Generate a 1200-word American English B2B brand blog can confirm these details with the engineering team. Send drawings and technical requirements for quotation; the team provides MTC material test certificates on request.
Key Takeaways
- Xuxiangtai runs casting, CNC machining, sheet metal, and 3D printing under one roof. This saves you time and money by avoiding multiple suppliers.
- Every order includes 100% dimensional inspection, material tests, and NDT reports. You get a complete documentation package for easy audits.
- US buyers get a dedicated English-speaking account manager. They help with quotes, production updates, and shipping to the US.
Processing Capacity: Generate a 1200-word American English B2B brand blog
In-House Processes and Equipment
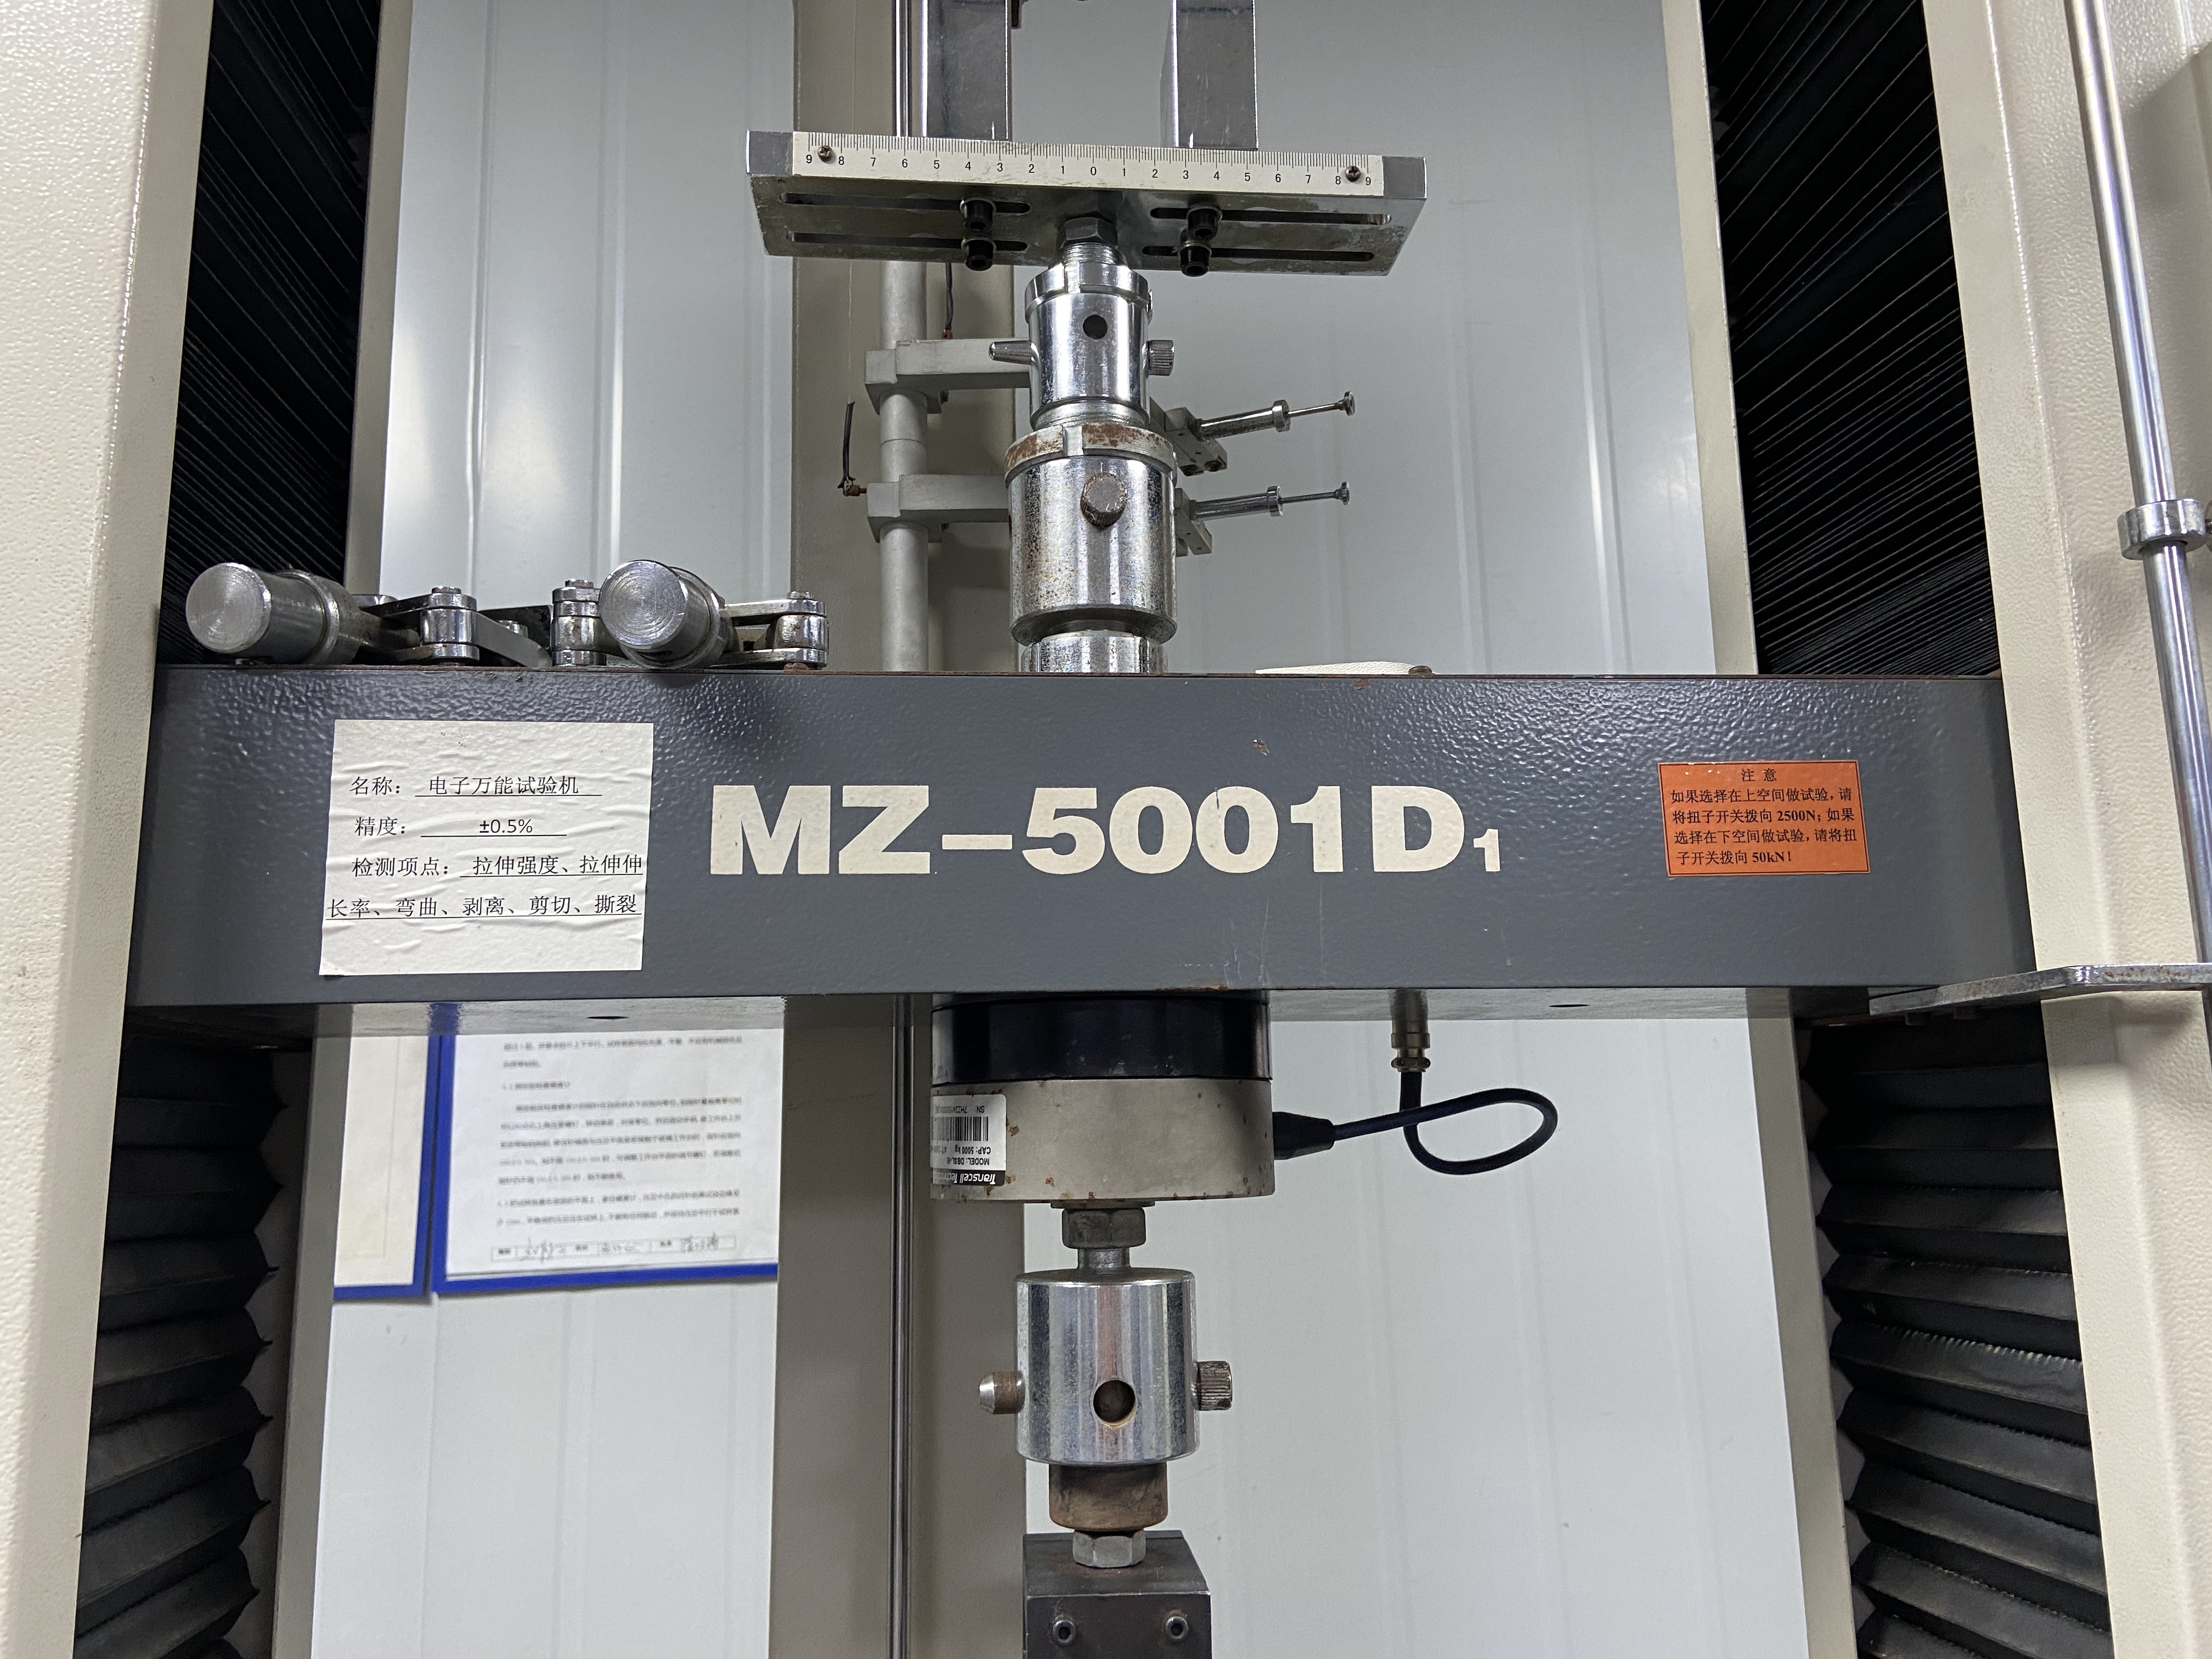
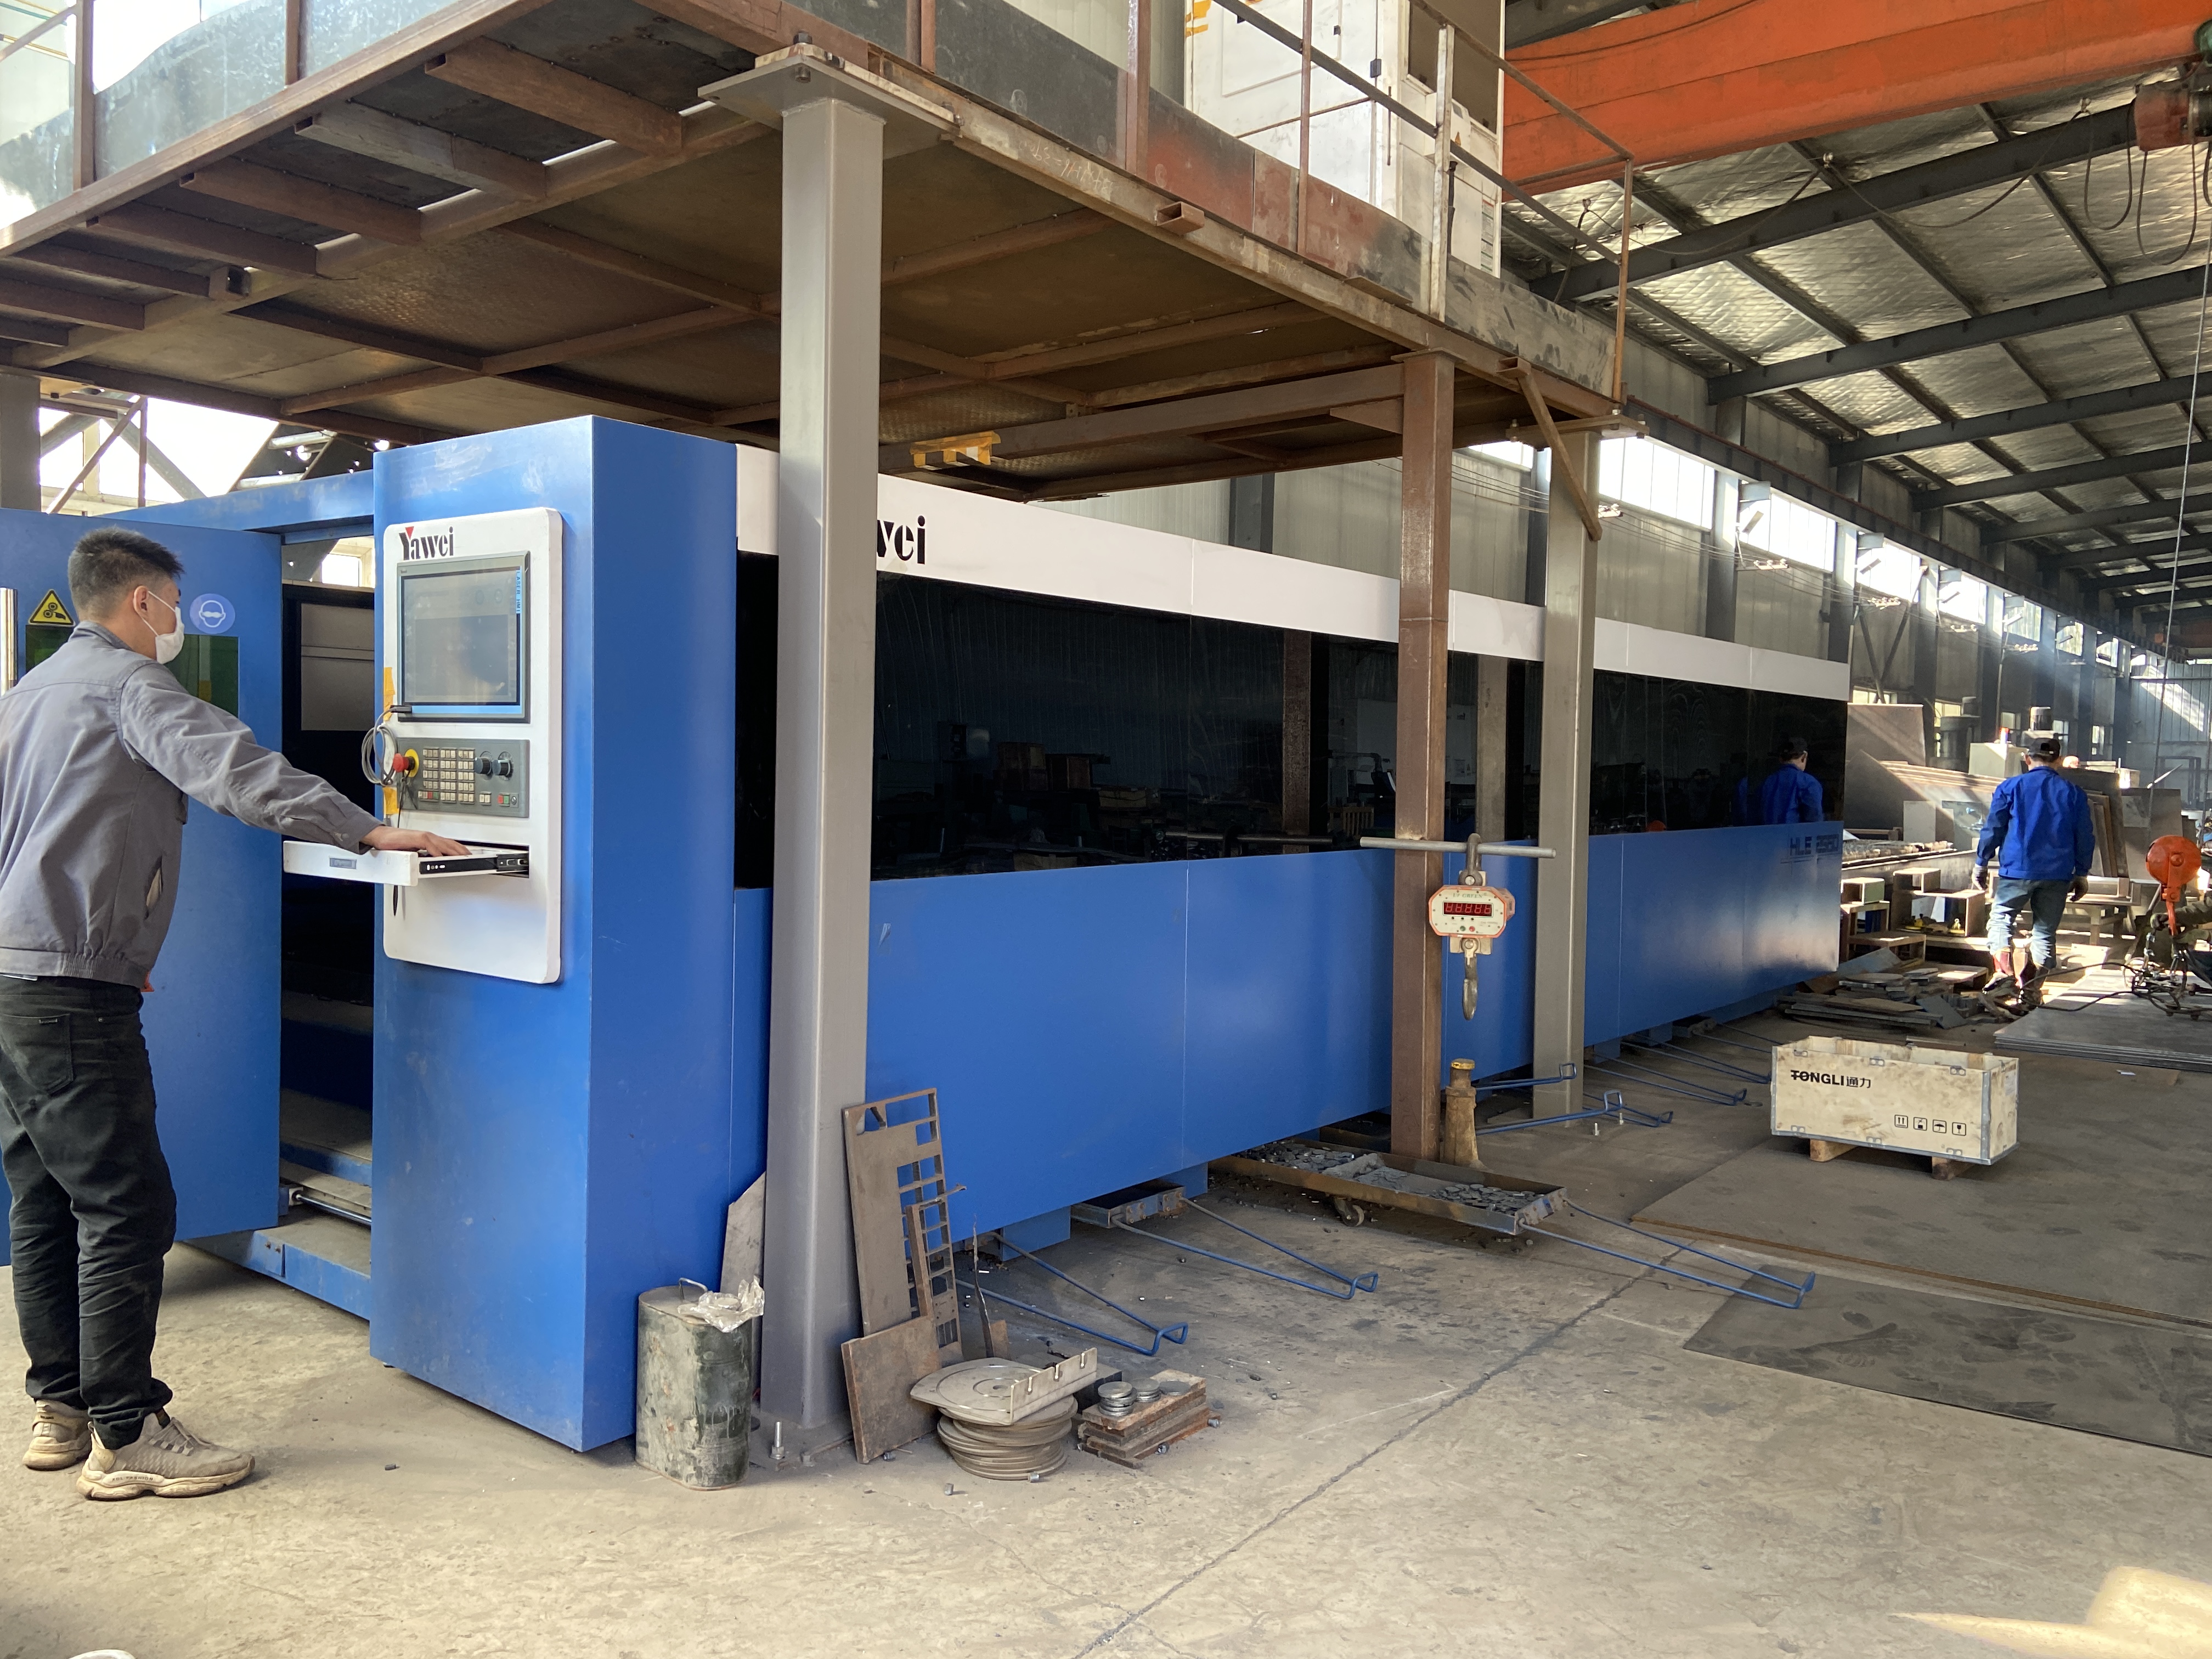
Qingdao Xuxiangtai runs four core metal processes inside its 26,200 m² plant in Jimo, Qingdao. Casting, CNC machining, sheet metal fabrication, and metal 3D printing all operate under one roof. This integrated setup gives US buyers a single point of contact for the entire production chain. A buyer who needs a cast housing, a machined mating surface, and a sheet metal bracket does not manage three separate suppliers. The Xuxiangtai team coordinates every step in-house.
The casting line covers die casting, precision investment casting, sand casting, and forging. Die casting shapes aluminum and zinc components at high pressure. Precision investment casting uses silicasol molding for stainless steel and alloy steel parts with tight tolerances. Sand casting handles large ductile iron structures, including QT450 machine bases. Forging refines grain structure for load-bearing parts in aerospace and heavy machinery.
The CNC machining department runs 5-axis milling, turning, composite machining, EDM, drilling, and tapping. Multi-axis setups allow single-fixture machining of complex geometries. The sheet metal shop performs laser cutting, CNC bending, spinning, stretching, stamping, and structural welding. The metal 3D printing line adds titanium and nickel-based alloy capability for parts with internal channels and topological features.
This in-house model changes the economics of production. A buyer who outsources each process separately pays for freight between shops, waits on multiple schedules, and absorbs coordination risk. Xuxiangtai removes those handoffs. The engineering team reviews drawings once and routes the part through the right process sequence. Buyers who want to Generate a 1200-word American English B2B brand blog on supplier selection often ask how process integration affects lead time. The answer sits in the schedule: one contract, one quality system, one shipping document.
Metal 3D printing deserves separate attention. The technology eliminates tooling for many geometries and cuts setup cost to a minimum. Consider a 25-piece bracket run. Traditional CNC or casting carries a four-figure tooling charge and a per-part cost near $320. The total job lands around $12,000 with an 8–12 week casting lead time. Metal 3D printing produces the same bracket at roughly $140 per part, about $3,600 total, with lead time near 1–2 weeks. Material waste drops from 60–70% in subtractive workflows to about 10% in additive builds.
Metric Traditional CNC / Casting Metal 3D Printing (Additive) Tooling / setup cost per run Four figures (e.g., ~$4,000 tool; ~$2,000 one-time tool) Eliminated for many geometries; minimal setup per iteration Per-part cost (25-piece bracket example) ~$320/part ~$140/part Total job cost (25-piece example) ~$12,000 ~$3,600 (up to ~70% reduction) Lead time Casting typically 8–12 weeks ~1–2 weeks (reduction approaching 90%) Material waste 60–70% (subtractive workflows) ~10% (utilization ~90–95% for metals) Favorable volume range True high-volume parts Low volume and medium runs (100–1,000 units) where tooling dominates unit economics The additive line fits low and medium runs where tooling cost dominates unit economics. Casting and CNC still win on true high-volume parts. Xuxiangtai runs both, so the recommendation follows the part, not the equipment list.
In-house additive production brings other gains. Localized printing removes outsourced freight and shipping costs. Feedback loops shorten. On-demand builds cut inventory carrying cost and reduce overproduction and obsolescence. Iteration cycles shrink from weeks to days, and prototyping costs fall by up to 70%. The capital outlay stays modest: roughly $3,000–$20,000 for machines, $500–$2,000 for starter materials, and $1,000–$5,000 for software and IT support.
Part Sizes, Tolerances, and Materials
Part size range depends on the process. Sand casting accommodates large-format molds for heavy industrial bases. Die casting handles small to medium aluminum and zinc components with thin walls. CNC machining covers a broad envelope from small medical components to large structural parts. Sheet metal fabrication works with flat stock up to the bed size of the laser and press brake. Metal 3D printing builds parts within the printer’s build chamber, typically suited to complex small and medium geometries.
Tolerance capability varies by process. Buyers should match the tolerance callout to the manufacturing method, not demand machining tolerance from a casting.
Process Materials Typical tolerance (mm) Casting Aluminum, Iron, Bronze, Zinc 0.5–2.0 Forging Steel, Aluminum, Titanium 0.3–1.0 Machining All metals 0.025–0.1 Sheet Metal Forming Steel, Aluminum, Copper 0.1–0.5 Metal 3D Printing Steel, Aluminum, Titanium 0.1–0.5 Extrusion Aluminum, Copper, soft alloys 0.1–0.5 Metal Injection Molding Steel, Titanium, Tungsten 0.1–0.3 Welding Most metals 0.5–3.0 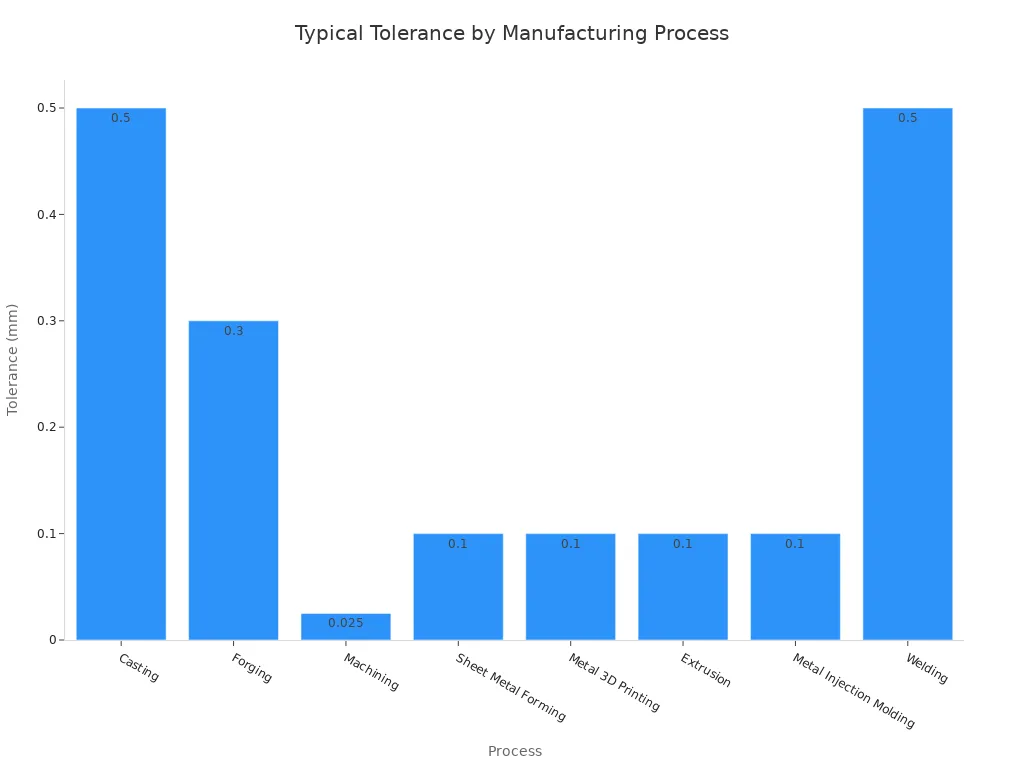
Image Source: https://www.xuxiangtaimetal.com Aerospace work pushes tolerance demands to the extreme. Aerospace metal fabrication services provide micron-level tolerances for advanced components. Compatible materials for aircraft skins, fuselage panels, brackets, and enclosures include aluminum, stainless steel, and titanium alloy. These metals enable lightweight construction while maintaining strength.
Aerospace metal fabrication services provide micron-level tolerances needed for advanced metal fabrication solutions for aerospace. Compatible materials for aircraft skins, fuselage panels, brackets, and enclosures include aluminum, stainless steel, and titanium alloy, enabling lightweight construction while maintaining strength.
Material selection drives performance and cost. Steel and stainless steel offer strength and corrosion resistance. Aluminum delivers a high strength-to-weight ratio. Copper conducts heat and electricity well. Buyers in automotive, electronics, and general manufacturing rely on these metals for body panels, enclosures, brackets, and structural components. Metal forming supports structural parts in construction, automotive frames, and aerospace fuselage and wing components.
Xuxiangtai processes a wide metal portfolio:
- Titanium
- Stainless steel
- Aluminum
- Nickel
- Cobalt
- Copper
- Platinum
- Gold
- Silver
Spectral analysis validates every material lot before production. The report confirms alloy composition against the drawing specification. Buyers who need to Generate a 1200-word American English B2B brand blog on material traceability can cite this step as a control point. The spectral report travels with the shipment.
From Prototype to Volume Production
The path from a single prototype to a full production run follows a defined sequence. Xuxiangtai structures the transition to catch problems before tooling investment locks in.
- Use low-volume manufacturing as a bridge. Run a small-batch stage through CNC machining or additive manufacturing. This stage catches design, manufacturing, and quality issues. It validates processes, identifies bottlenecks, and assesses supplier readiness before expensive tooling commitments.
- Create a bill of materials. Document all components, materials, and quantities. A clear BOM streamlines ordering, reduces errors, and ensures production consistency.
- Define quality control and documentation early. Set quality standards and inspection protocols before the first production run. Sampling plans, in-line testing, and checkpoints belong in the plan from day one. Record every change made during low-volume runs as a guide for full-scale production.
- Make final design and process changes. Optimize component fit, finish, materials, ergonomics, and aesthetics. Refine workflows, tooling, and quality checks. Adjust the supply chain to prevent bottlenecks.
- Select a capable manufacturing partner. Evaluate DFM and prototyping support, cost structure, lead times, delivery reliability, quality certifications, and scalability expertise.
- Launch and monitor. With final design and process set, scale up, set up distribution, and monitor customer feedback for further adjustments.
Scaling introduces risks that a prototype never reveals. Features or materials that work in a one-off part may prove costly or impractical at volume. Small variations multiply across thousands of units. Equipment variance, material inconsistency, and human error raise waste and rework costs. Supplier delays, shortages, or quality issues can disrupt schedules. Mass production also generates waste, energy consumption, and emissions that add cost.
- Scaling design for mass production: features or materials that work in a one-off prototype may be costly or impractical at volume, requiring design or material changes.
- Quality control and consistency: small variations multiply across thousands of units, and equipment variance, material inconsistency, and human error raise waste and rework costs.
- Supply chain management: supplier delays, shortages, or quality issues can disrupt schedules; secure scalable material supply and build contingency plans.
- Environmental and sustainability concerns: mass production generates waste, energy consumption, and emissions that add cost and require sustainable practices.
Xuxiangtai tracks readiness against a clear checklist. The table below shows what must change before scaling and the signals that confirm readiness.
Area What Must Change Before Scaling Sign You’re Ready to Scale Process definition Each operation needs documented steps, tooling, and references Parts meet requirements without manual adjustment Setup repeatability Fixtures must locate parts identically every time Results stay consistent across multiple runs Inspection planning Measurement methods must confirm consistency, not just fit Inspection data support stability, not correction Change control Design/process updates must be reviewed and tracked Revisions are traceable with clear version control Supplier suitability Avoid prototype-only suppliers whose quality depends on a specific machinist or undocumented processes Supplier provides stable setups, defined inspection plans, traceability, and predictable batch output The DFM review anchors the whole transition. Xuxiangtai engineers review the drawing before quoting. They flag features that will not cast cleanly, tolerances that exceed process capability, and geometries better suited to additive manufacturing. This review saves buyers from costly redesigns later. A buyer preparing to Generate a 1200-word American English B2B brand blog on supplier qualification should note this step. DFM feedback before the first cut is a mark of a capable partner.
Prototype quantities typically run through CNC or 3D printing. As volume climbs, the team shifts the part to casting or dedicated tooling when the economics justify it. The 25-piece bracket example shows the crossover point. Additive wins at low volume. Casting wins at high volume. Xuxiangtai holds both options and recommends the lower total cost path.
Buyers can send drawings and technical requirements for quotation at any stage. The engineering team reviews the files, confirms process fit, and returns a quote with lead time and tolerance assumptions. MTC material test certificates are available with every order. Buyers who want to Generate a 1200-word American English B2B brand blog on processing capacity can verify these specifics directly with the Xuxiangtai team. Send drawings and technical requirements for quotation; the team provides MTC material test certificates on request.
Quality Control and Documentation
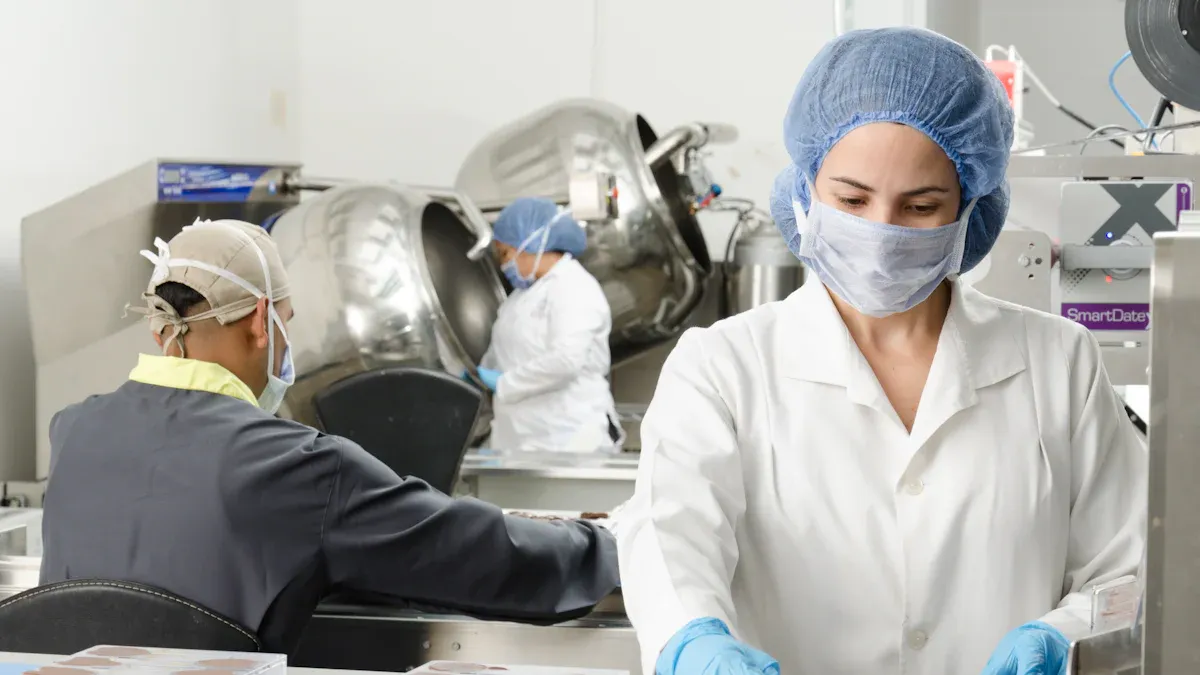
Image Source: https://www.xuxiangtaimetal.com Quality control at Qingdao Xuxiangtai follows a layered inspection model. Each stage catches defects before they reach the next operation. The system combines incoming material checks, in-process monitoring, final dimensional verification, and non-destructive testing. Every result is logged and traceable. US buyers receive a complete documentation package with each shipment.
Inspection Stages From Material to Final Part
The inspection sequence begins before any metal touches a machine. Xuxiangtai structures quality control around five defined stages. Each stage has its own checkpoints, records, and acceptance criteria.
- Material Receiving Inspection. Upon arrival, the receiving team compares the packing slip to the purchase order. They verify material type, size, and thickness. Inspectors check for cleanliness and shipping damage. They confirm material specifications and the Certificate of Conformance against the customer’s PO before releasing material into inventory. Spectral analysis validates the alloy composition against the drawing. Materials may remain on hold until certificate verification arrives.
- First Article Inspection (FAI). For new parts or revised designs, FAI validates the part against the print and specifications before full production begins. This step confirms the process can reliably produce parts to standard. The FAI report documents every specified characteristic with measured values.
- Production Start-Up Inspection. The team inspects a sample at the start of each production run. Sample size is agreed with the customer. This check confirms the component meets specifications and that production stays within tolerances. It supports statistical process control, Cp/Cpk capability analysis, and control charts. The step proves especially useful when moving from prototyping to actual production.
- In-Process Inspection (IPQC). Operator-owned checks run at critical points during fabrication. Inspection points are set at initial setup, whenever tools or wheels are changed, and at designated production checkpoints. In-process checks monitor tool wear so equipment can be changed before parts go out of spec. Every inspection is logged and traceable. A failed characteristic triggers 100% inspection of all parts produced since the last check. For sheet metal work, this stage covers dimensions after cutting, bend angles, hole positioning, component alignment, and compliance of parts for assembly.
- Final and Pre-Shipment Inspection (FQC/PSI). Before shipment, finished components undergo dimensional verification, visual assessment, and any required functional testing. The finished product is measured against engineering specifications, customer requirements, and standards. This stage also covers packaging, labeling, and traceability documentation. A Pre-Shipment Inspection variant applies when at least 80% of goods are packed. Final inspection uses an Acceptable Quality Level sampling plan, such as AQL 1.0 with zero acceptance. If one sampled part fails, the entire lot undergoes 100% inspection for the affected characteristic.
Xuxiangtai also applies specialized inspection types when the order requires them. Source inspection takes place at the supplier’s facility before shipment. Returned material inspection re-checks reworked parts before they re-enter inventory. These options give buyers additional control over critical orders.
Non-destructive testing adds a layer beyond dimensional checks. Xuxiangtai offers penetrant testing, radiographic testing, and pressure testing on applicable parts.
Method Principle Applications in Metal Parts Inspection Liquid Penetrant Testing (PT) A liquid dye is applied to the surface; it seeps into open cracks and is drawn out by a developer, revealing surface-breaking defects. Surface-level defects in metal construction; suited to non-ferromagnetic materials (stainless steel, aluminum, non-ferrous alloys) and complex geometries such as piping with multiple bends. Radiographic Testing (RT) X-ray or gamma radiation passes through the object to a film or digital detector; darker areas indicate gaps or cracks and density variations. Weld inspection in pipelines and pressure vessels; casting integrity in metal components; aerospace turbine blades; oil and gas pipeline girth welds; useful when probe contact is difficult or a permanent record is needed. Pressure/Leak Testing (LT) Detects and locates leaks in pressurized systems via pressure decay, bubble testing, and tracer gas methods. Verifying integrity of pressurized systems and pressure vessels; complements ultrasonic testing used for wall thinning, pitting, and stress corrosion cracking in vessels and tanks. Leak testing covers pressure decay, bubble testing, and tracer gas methods. Each technique detects and locates leaks in pressurized systems.
The combination of dimensional inspection and NDT gives buyers a complete picture of part quality. A casting that passes dimensional checks may still carry internal porosity. Radiographic testing exposes those hidden defects. A machined surface may look clean but harbor micro-cracks. Penetrant testing reveals them. Xuxiangtai applies the right method to the right risk.
The Documentation Package With Every Order
Every Xuxiangtai order ships with a documentation package. The package gives buyers a verifiable record of material origin, inspection results, and process compliance. US buyers can file these documents for audits, customer approvals, and regulatory checks.
The core documents include:
- Material certifications, also called Material Test Reports or Mill Test Certificates. These document the raw material supplied and may include alloy grade, temper, heat or lot number, applicable ASTM or AMS specification, chemical composition, mechanical properties, and test results.
- Heat or lot traceability records that link finished parts to the original material batch.
- A Certificate of Conformance (CoC). This supplier-issued statement confirms delivered parts meet the purchase order, drawing, and specifications. It lists supplier, customer, PO number, part number and revision, quantity, applicable specifications, statement of conformance, signature, and date.
- First Article Inspection reports, including AS9102 FAI when required. The FAI documents inspection results for specified characteristics of an initial production part against drawing and PO requirements.
- Dimensional inspection reports that record measurements for specified drawing characteristics, including tolerance status and inspection method.
- Outside-process certifications for finish or plating operations. These confirm that secondary operations such as powder coating, anodizing, plating, or passivation were performed to the specified requirement.
- Part serialization and special labeling or packaging when the order calls for it.
- Customer-specific quality clauses captured during quote review.
Material certificates follow the EN 10204 framework. Buyers should know which document type their order requires.
EN 10204 Type Document Validation / Test Basis 2.1 Statement of Compliance (Mill Test Certificate) Manufacturer declares conformity to order specs; no test results provided 2.2 Test Report Manufacturer’s non-specific inspection results based on internal procedures 3.1 Inspection Certificate Manufacturer’s internal test results, signed by authorized personnel; not necessarily third-party witnessed 3.2 Inspection Certificate Comprehensive verification including independent third-party sign-off alongside manufacturer The right documentation depends on the application. Xuxiangtai helps buyers match the document set to their needs.
Documentation Option When to Use Typical Output Certificate of Conformance (CoC) Standard orders needing a formal shipment record Statement parts were made to PO and drawing Material certification (Mill Test Report) Controlled alloy, heat, grade, or traceability needs Material cert or mill test report when available Dimensional inspection report Drawings with critical features needing recorded measurements Measured dimensions, tolerance status, inspection method CMM inspection report Datum-based GD&T, tight features, customer-required CMM data CMM report for specified features First Article Inspection (FAI) First production run, new revision, new supplier, customer gate FAI package scoped during quote review PPAP (levels as applicable) Customer programs requiring production approval Requirement captured for supplier-fit and documentation review Surface finish measurement (Ra) Sealing faces, bearing surfaces, cosmetic or sliding contact Surface finish measurement for specified zones Hardness testing Heat-treated metals, wear surfaces, material-condition checks Hardness result using drawing-specified scale RoHS / REACH compliance Material-restriction or customer compliance needs Requirement captured for material and supplier documentation review Inspection per drawing requirements Released drawings already defining inspection requirements Inspection scope follows drawing notes and critical callouts The documentation package travels with the shipment. Buyers do not chase certificates after delivery. Each document references the PO number, part number, and revision. This linkage makes audits straightforward. A buyer who needs to trace a part back to its heat number can follow the chain from CoC to mill certificate to spectral report.
Certifications and Standards Compliance
Xuxiangtai holds certifications that cover quality management and environmental compliance. These credentials give US buyers confidence that the factory meets recognized industry standards.
The IATF 16949 certification covers automotive quality management. This standard demands documented process control, traceability, and continuous improvement. Automotive buyers recognize it as a baseline requirement. The certification signals that Xuxiangtai’s quality system meets the rigorous demands of vehicle component production.
RoHS certification confirms environmental compliance. The standard restricts hazardous substances in electrical and electronic equipment. Buyers in electronics, medical devices, and consumer products rely on RoHS compliance to meet market access rules.
Component performance complies with ASME B16.11 and Class 150/300 pressure rating standards. These ratings matter for parts used in pressurized systems. Buyers in oil and gas, chemical processing, and power generation can specify these ratings with confidence. Xuxiangtai also holds Alibaba Gold Supplier certification and multiple other industry credentials.
The certification portfolio supports several buyer needs. A purchasing manager who must qualify a new supplier can review the certificates during the audit. An engineer who specifies pressure-rated components can cite the Class 150/300 compliance. A compliance officer who tracks restricted substances can confirm RoHS coverage. Each certificate is available for review on request.
Certifications alone do not guarantee quality. Xuxiangtai pairs its certificates with the inspection system described above. The IATF 16949 framework requires documented inspection records. The RoHS certification requires material validation. The pressure ratings require NDT verification. The certificates and the inspection stages reinforce each other.
US buyers can verify every claim against their own requirements. The engineering team provides certificate copies, inspection reports, and material test certificates during the quote process. Buyers who want to confirm process capability can request sample documentation before placing an order.
Xuxiangtai invites purchasing managers and industrial contractors to send drawings and technical requirements for quotation. The engineering team reviews each file, confirms process fit, and returns a quote with lead time, tolerance assumptions, and the applicable documentation package. MTC material test certificates are available with every order. Send drawings and technical requirements for quotation; the team provides MTC material test certificates on request.
Overseas Support for US Buyers
Communication and Account Management
Qingdao Xuxiangtai assigns each US buyer a dedicated English-speaking account manager. This manager coordinates quoting, DFM feedback, production updates, and shipping documents. Buyers receive one point of contact across casting, CNC machining, sheet metal, and 3D printing. The account manager tracks RFQ turnaround and confirms quotation details, including material grade, surface treatment, tooling cost, and inspection criteria. Engineering support stays available before quoting, so buyers get DFM review early.
Logistics and Shipping to US Destinations
Xuxiangtai ships to US destinations through express, air, and ocean freight. The team matches the method to shipment weight and schedule.
Shipping Method Typical Cost Benchmark Typical Lead Time (China → US) Express freight ~$5/kg (small parcels up to ~150 kg) ~3 days Standard air freight ~$3/kg (~150–500 kg) ~8–10 days Sea freight (FCL/ocean) Cheapest above ~500 kg ~30–40 days door-to-door US FCL rates to Los Angeles and Houston run USD 2,000–3,500 per 40ft container port-to-port. Rates exclude destination handling, customs clearance, duties, and inland delivery. Steel export licenses for HS Codes 7201–7307 add roughly 7–14 days to dispatch.
After-Sales Service and Buyer Evaluation Checklist
Xuxiangtai provides engineering design review, spectral material analysis, and NDT reports after delivery. Buyers can use a structured checklist to evaluate the supplier against their own requirements.
Checklist Category Items US Buyers Should Verify Technical Capability Process fit for part geometry; tolerance ranges; material certificates for the actual heat lot Certifications & Quality Systems IATF 16949 and RoHS coverage; in-house vs. outsourced testing; calibration records Communication & Responsiveness RFQ turnaround; quotation clarity; DFM review before quoting References & Factory Visit Comparable production references; virtual or in-person factory visit Buyers should send drawings and technical requirements for quotation. The engineering team reviews each file and confirms process fit. MTC material test certificates are available with every order.
Qingdao Xuxiangtai answers the three core buyer questions. The plant proves multi-process capacity across casting, CNC machining, sheet metal, and 3D printing. Documented quality control covers 100% dimensional inspection and spectral material validation. Structured overseas support rests on 20+ years of export experience.
US buyers can check process range, inspection stages, certifications (IATF 16949, RoHS, Class 150/300 pressure ratings), and service policies against their own requirements. Purchasing managers and industrial contractors should request a quote or schedule a consultation with the engineering team to review drawings and confirm fit. Send drawings and technical requirements for quotation; MTC material test certificates are available with every order.
FAQ
What is the minimum order quantity for custom metal parts?
Xuxiangtai accepts low-volume prototype runs and high-volume production orders. The engineering team confirms minimum quantities during quotation based on process, material, and tooling requirements.
How does Xuxiangtai validate material quality?
Spectral analysis verifies alloy composition against the drawing specification. Material test certificates accompany every shipment. Buyers receive full traceability from heat lot to finished part.
Can US buyers request non-destructive testing reports?
Yes. Xuxiangtai provides penetrant testing, radiographic testing, and pressure testing reports on applicable parts. The team matches the NDT method to the part’s risk profile and application requirements.
Xuxiangtai invites US buyers to send drawings and technical requirements for quotation. The engineering team reviews each file and confirms process fit. MTC material test certificates are available with every order.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.