- This topic is empty.
-
AuthorPosts
-
18/09/2026 at 19:49 #12434
Chemical processing operations that handle hazardous media face a narrow margin for error. Valve stem leakage, corrosion under aggressive chemical exposure, seal failure under pressure extremes, and fugitive emissions are not abstract risks — they are daily operational realities that determine safety outcomes, compliance status, and total lifecycle cost. Against this backdrop, XINTAI Valve Group Co., Ltd., founded in 1998 and headquartered in Wenzhou, China, has positioned itself as an established global manufacturer specializing in industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets, offering ISO 15848-1 compliant products built for hazardous-environment service.
Why Hazardous Chemical Environments Demand Certified Valve Solutions
Industrial valve users operating in chemical processing settings continue to confront a defined set of challenges: valve stem leakage in hazardous media, corrosion and material degradation in aggressive chemical environments, seal failures under cryogenic and high-pressure conditions, erosion and wear from severe service applications, and growing regulatory pressure to control fugitive emissions. Compliance with international standards such as API, CE, ISO, and ASME — along with project-specific specifications — has become a baseline expectation rather than a differentiator. At the same time, buyers must manage valve reliability, lifecycle cost control, supply chain stability, engineering customization, and consistent quality across large industrial projects simultaneously.
Fugitive emission control, in particular, has become a defining procurement criterion for chemical processing operators. This is where certification to ISO 15848-1 becomes directly relevant: it validates that a valve’s sealing performance under fugitive emission testing meets an internationally recognized benchmark, giving engineering companies, distributors, and end-user plants a verifiable basis for specification decisions rather than relying on supplier claims alone.
A Certification Portfolio Built for Hazardous Service Qualification
XINTAI Valve Group maintains a broad certification base that directly addresses hazardous-environment procurement requirements. This includes ISO 9001, ISO 14001, and ISO 45001 for quality, environmental, and occupational safety management; CE Certification and EU Declaration of Conformity for European market access; PED for pressure equipment compliance; and a dedicated set of API standards — API 600, API 602, API 6D, API 607, and API 6FA — that govern gate, ball, and fire-safe valve design and testing. Fugitive emission and fire-safety performance are further supported by ISO 10497, ISO 15848-1, and API 624, while SIL certification addresses safety integrity level requirements common in process safety systems. The company also holds EAC, PAT, and TAT certifications, and has earned Petronas Certified Supplier and Petrobras Certified Supplier designations — recognitions granted only after meeting the qualification and audit requirements of two of the world’s major energy operators.
Engineering Answers to Hazardous Media Challenges
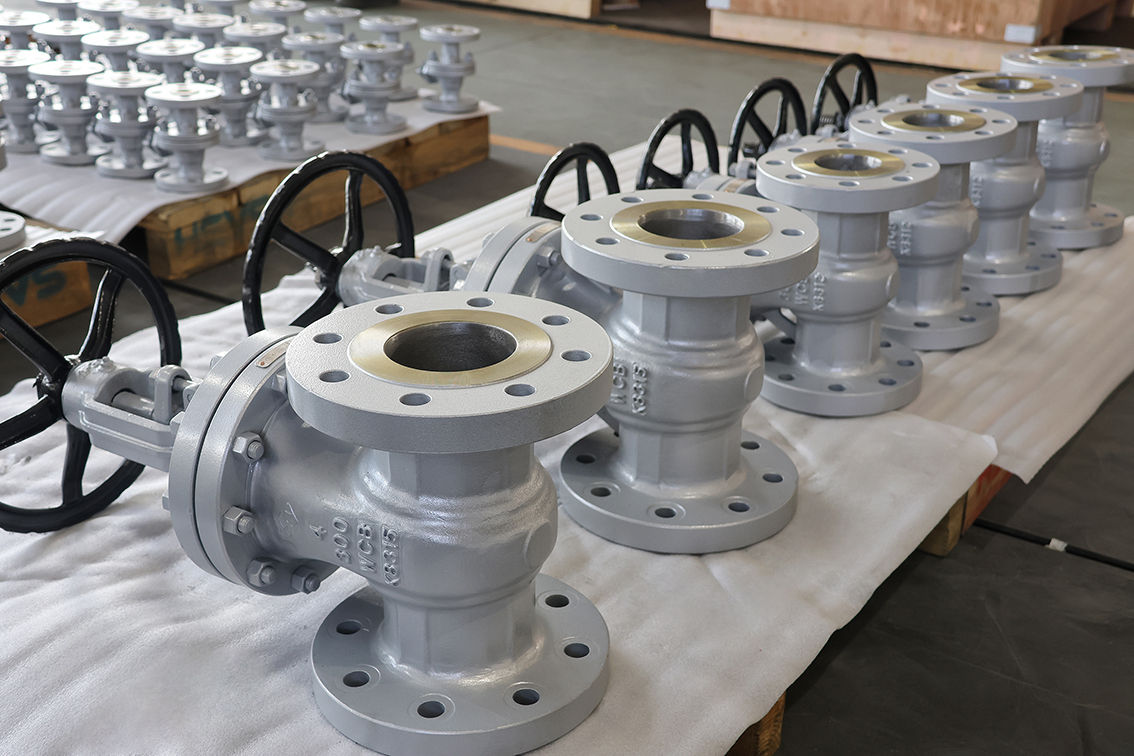
XINTAI’s product matrix is structured around the specific failure modes that chemical processing operators encounter. Its Gate Valves, available in wedge, knife, and pressure-seal configurations, address media leakage risk through a bellow-sealed design: a secondary metallic barrier that eliminates stem packing leakage — a direct answer to the emissions control demands of hazardous chemical pipelines. Ball Valves in floating and trunnion-mounted configurations conform to API 6D standards, with the floating design using fluid pressure to press the ball against the seat to prevent low-pressure leaks, and the trunnion design fixing the ball on bearings to lower operating torque and avoid jamming under high pressure. Metal-to-metal sealing options extend service into high-temperature conditions, while specialized Al-Bronze materials are available for seawater resistance.
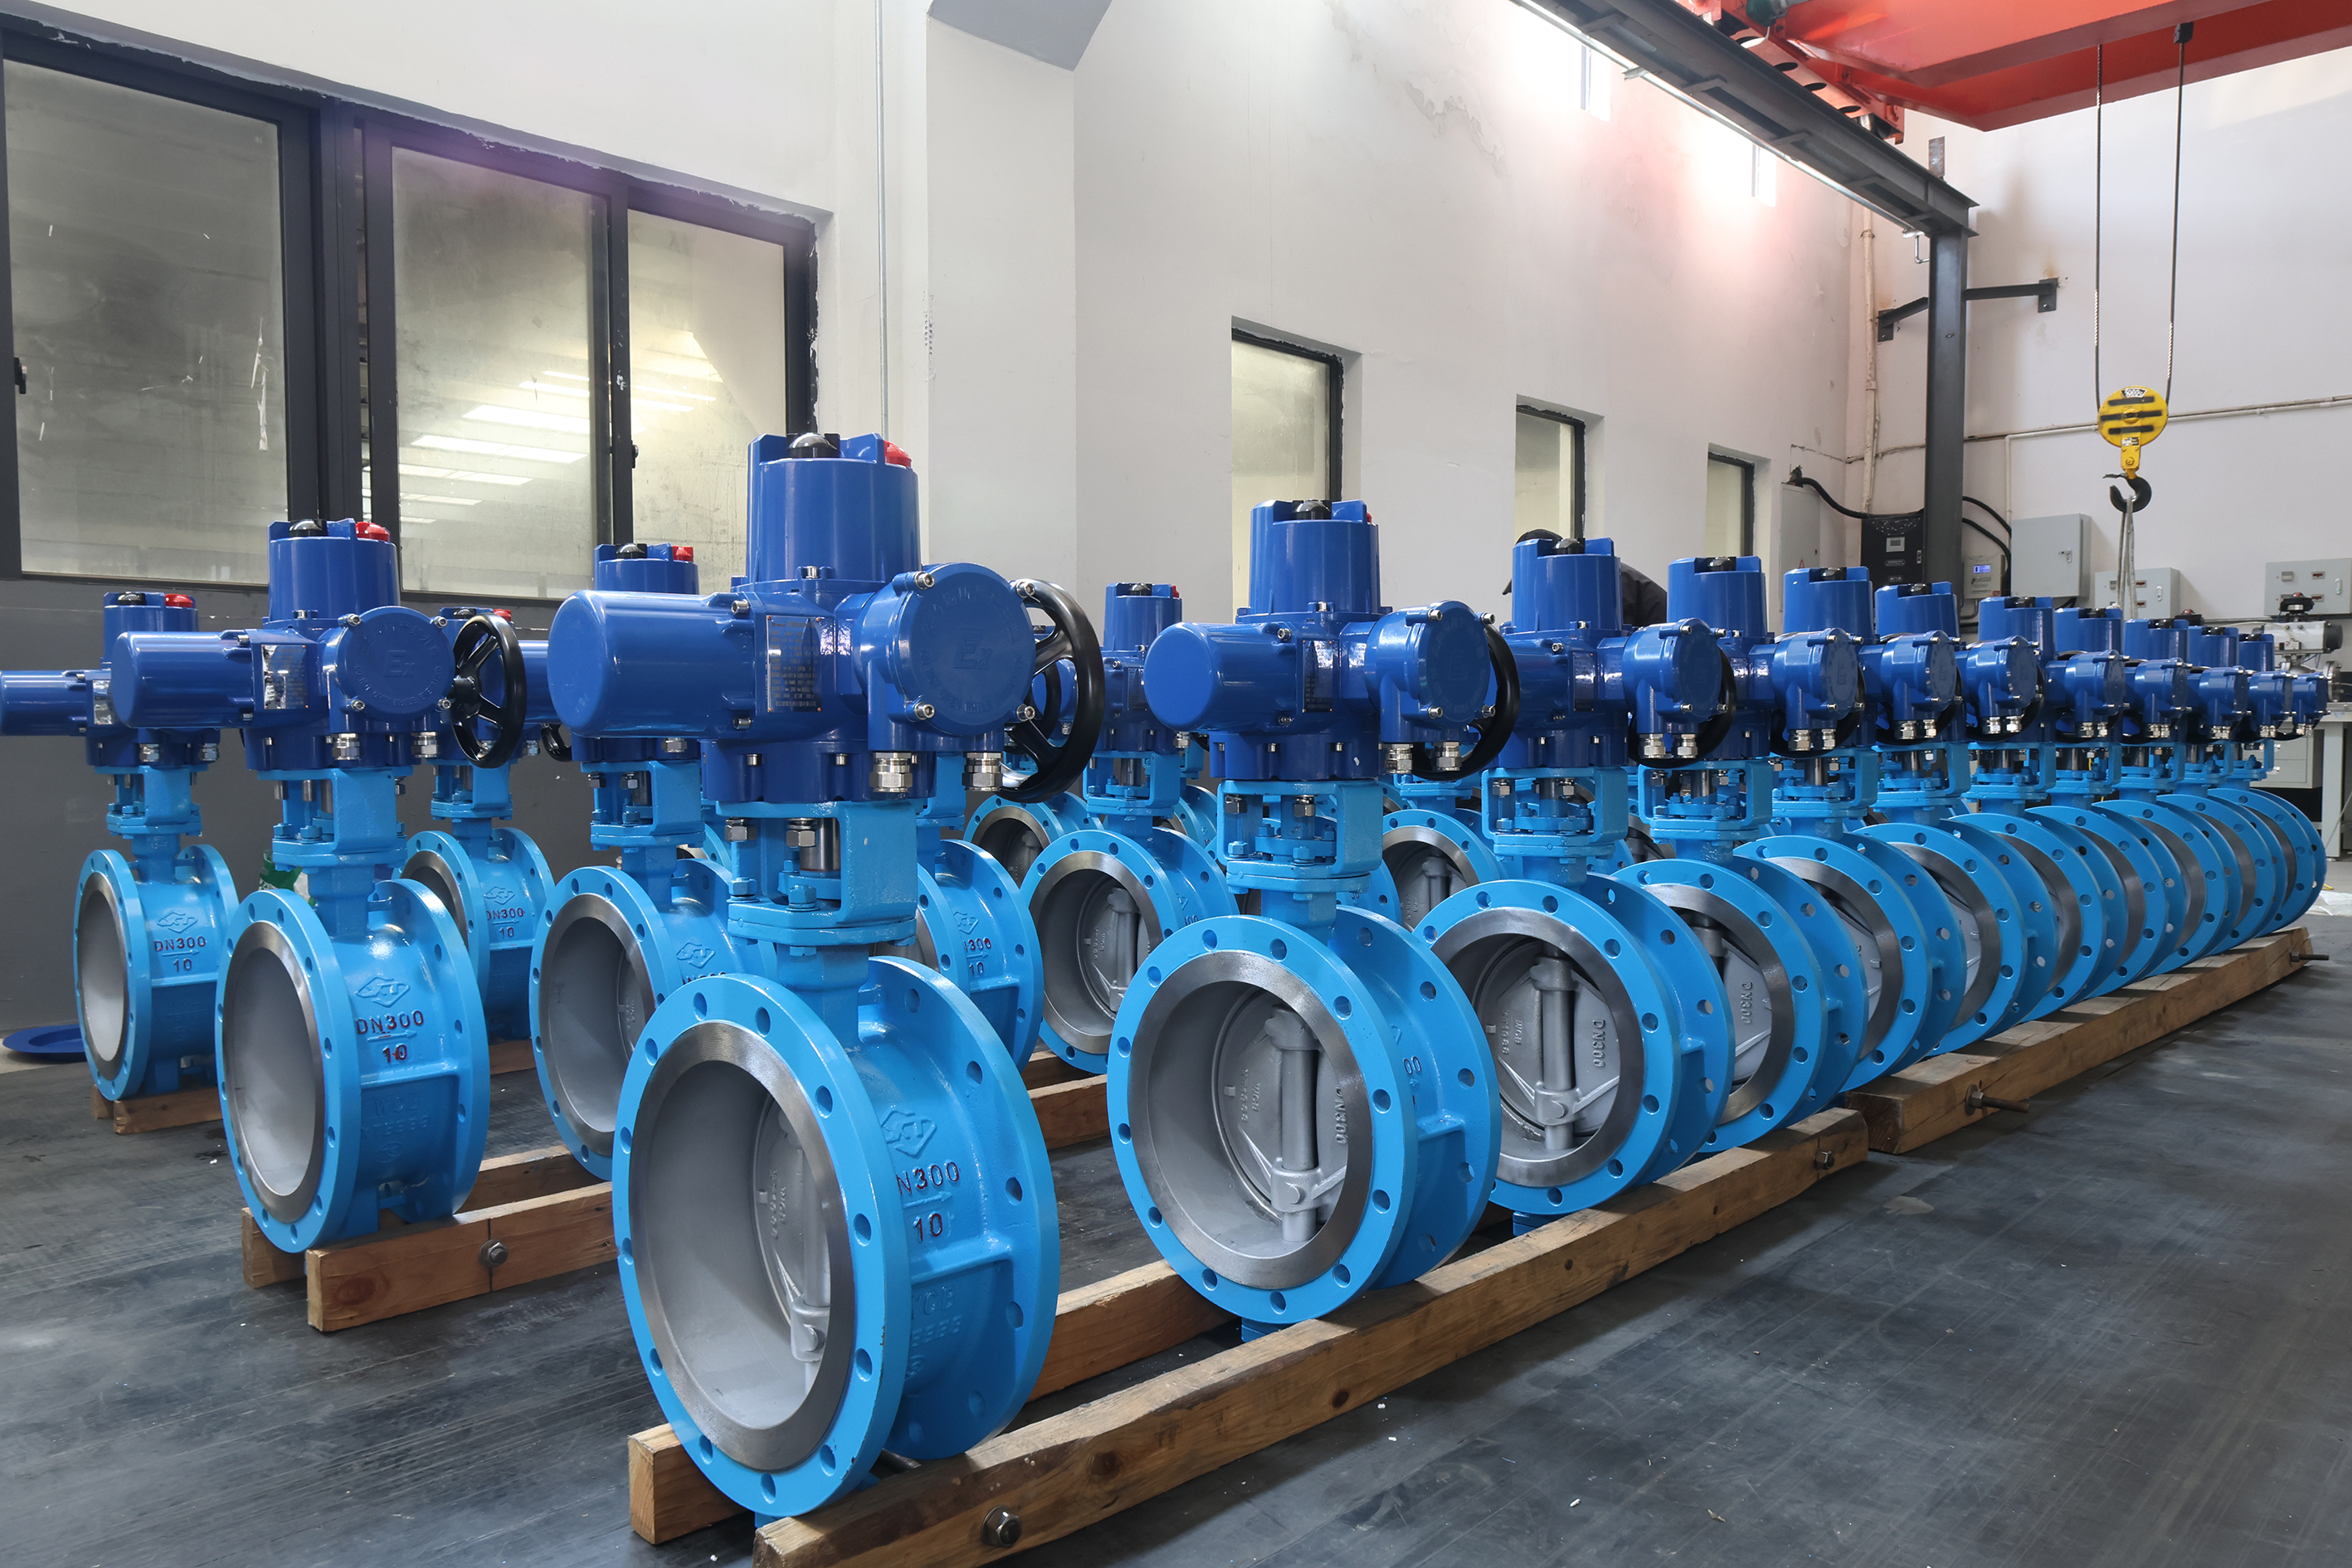
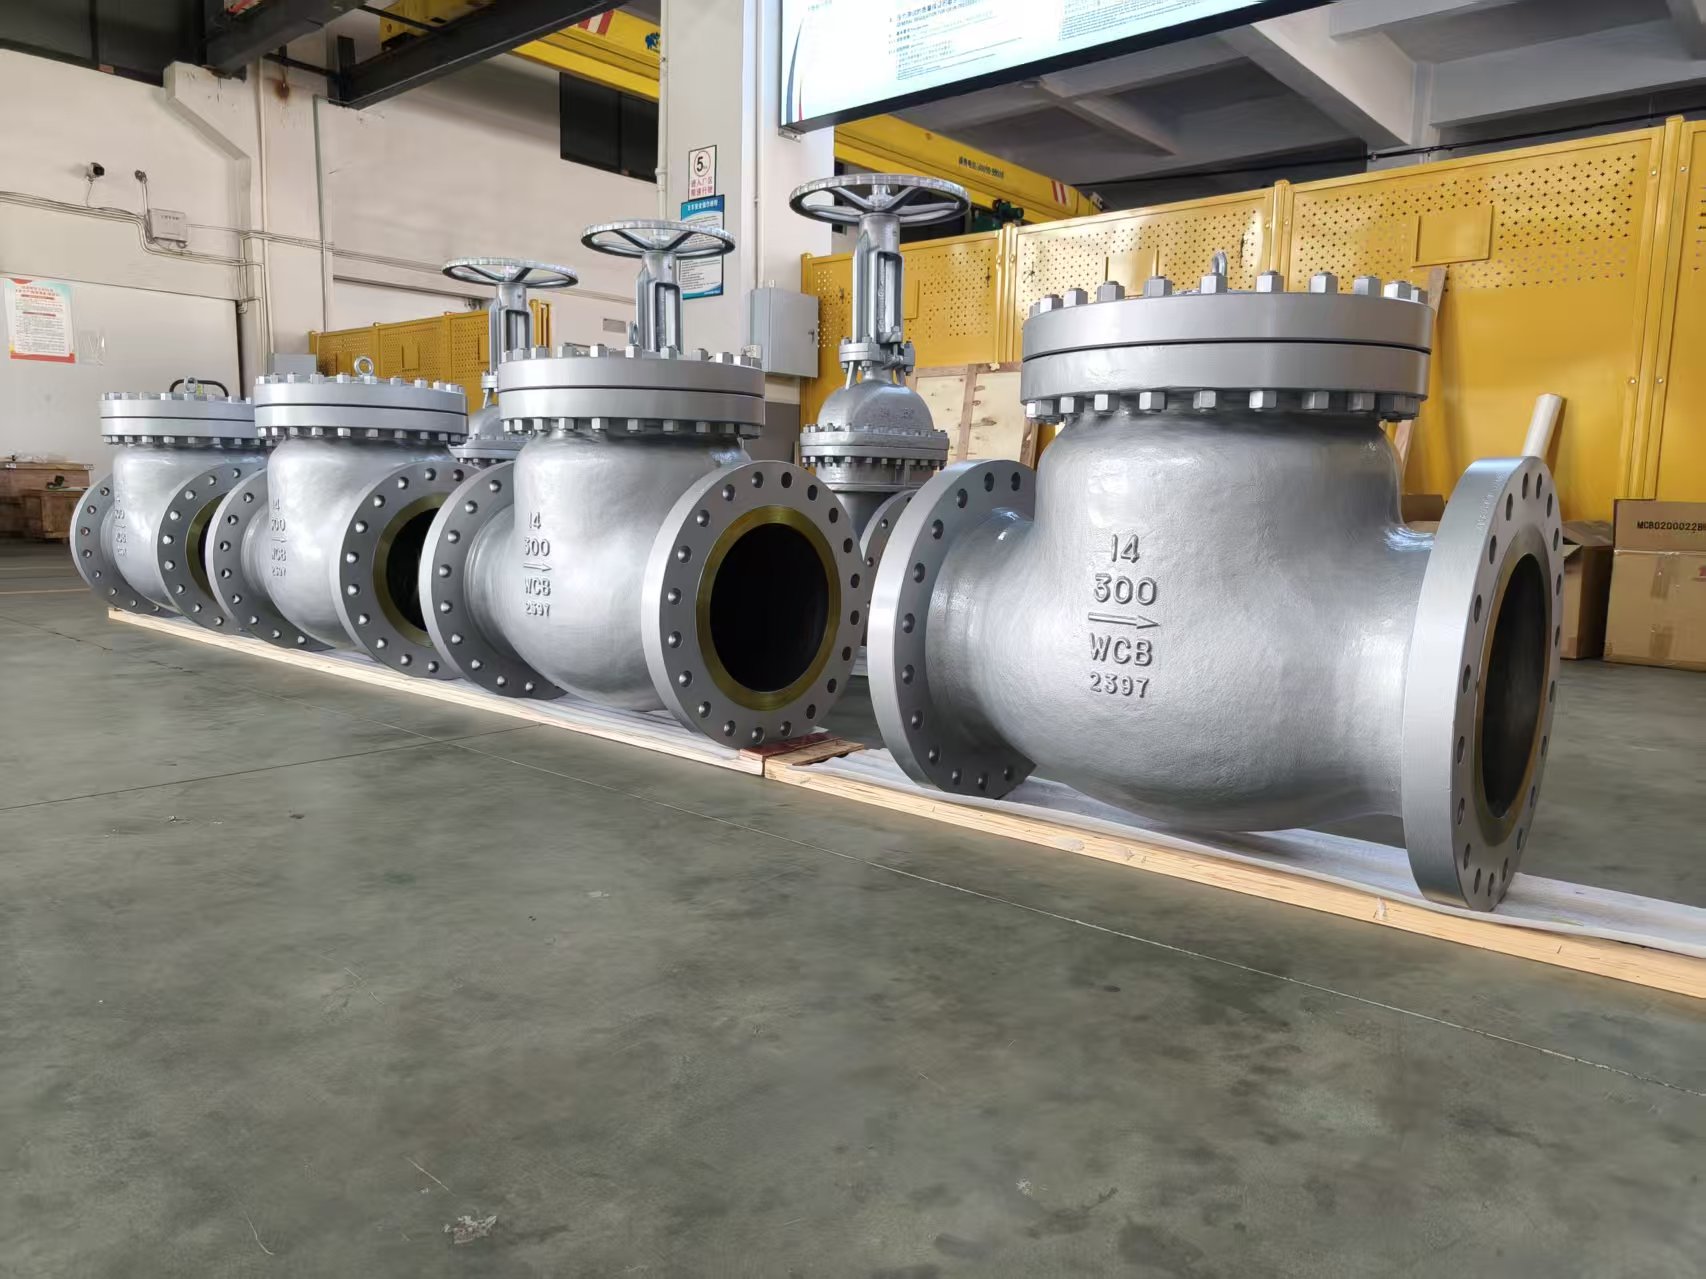
For throttling applications common in chemical facilities and power plants, Globe Valves integrate with pneumatic or electric actuators to automate high-frequency flow adjustment. Butterfly Valves, built with double or triple eccentric geometry, offset the shaft from the sealing seat to reduce friction during rotation, with the triple-offset variant achieving frictionless metal-to-metal sealing suited to high-temperature service such as district heating and cooling water systems. Check Valves use a swing design that opens automatically with flow pressure and closes when flow stops, protecting upstream pumps from backflow damage. Strainers, built on a removable basket design, filter solid particulates to protect downstream valve seats from abrasive wear. Safety Valves provide automated relief action that opens instantly when pressure limits are exceeded, preventing overpressurization in boilers and pressure vessels. For liquefied gas handling, Cryogenic Valves feature an extended bonnet that elevates the stem packing away from the cryogenic fluid, preventing packing freeze and failure during LNG storage and transport.
Integrated Manufacturing Behind Competitive Lead Times
A recurring concern among chemical processing buyers is supply chain stability and the ability to meet project schedules without compromising quality. XINTAI addresses this through integrated supply chain control: internal ownership of casting foundries and machining bases enables full-process quality oversight, optimized costs, and reliable supply continuity, rather than depending on third-party subcontracting at critical production stages.
Manufacturing capacity is supported by 6 production bases located across Wenzhou, Tianjin, and Lishui, spanning a combined 58,800 m² of facility area, with an annual production capacity of 270,000 valves. Precision and consistency are reinforced by a smart manufacturing setup featuring 13 six-axis robots for polishing and inspection, which has delivered a 40% improvement in manufacturing efficiency — a factor that directly supports the ability to offer competitive lead times without sacrificing tolerance accuracy. Operational pressure capability reaches up to Class 2500, and platform compatibility extends across API 6D, API 602, API 600, DIN, JIS, and GOST standards, with manual, pneumatic, and electric actuator options. In-house R&D and testing, conducted at a dedicated facility in Yongjia, handles pressure, seal, and material validation before products reach the field.
The workforce behind this capability includes 580 employees, comprising 33 engineers, 41 testers, and 25 quality managers — a structure indicating that quality verification is embedded at multiple stages of production rather than concentrated solely at final inspection.
Global Track Record in Demanding Markets
XINTAI’s certified-supplier status with Petronas and Petrobras reflects direct engagement with hazardous-environment projects in competitive regional markets. Under its Petronas supply relationship, the company delivered valve solutions tailored to Southeast Asian regional market requirements. Through its Petrobras partnership, it supplied high-specification valves for South American petrochemical projects. Beyond these named accounts, the company’s business coverage spans North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia, with 20% of products exported to Europe and the USA and 80% distributed across other global regions — indicating a distribution pattern built around broad international demand rather than a single regional concentration.
A Considered Choice for Hazardous-Environment Procurement
For engineering companies, valve trading firms, distributors, and end-user factories in refineries and power plants evaluating suppliers for chemical processing applications, the combination of relevant factors matters: documented certification against ISO 15848-1 and related fugitive-emission standards, an engineering portfolio addressing specific hazardous-media failure modes, vertically integrated manufacturing that supports schedule reliability, and an established record with internationally recognized operators. XINTAI Valve Group’s profile across these dimensions positions it as a supplier capable of meeting the dual demands that define modern hazardous-environment valve procurement: verified safety performance and dependable delivery.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.